
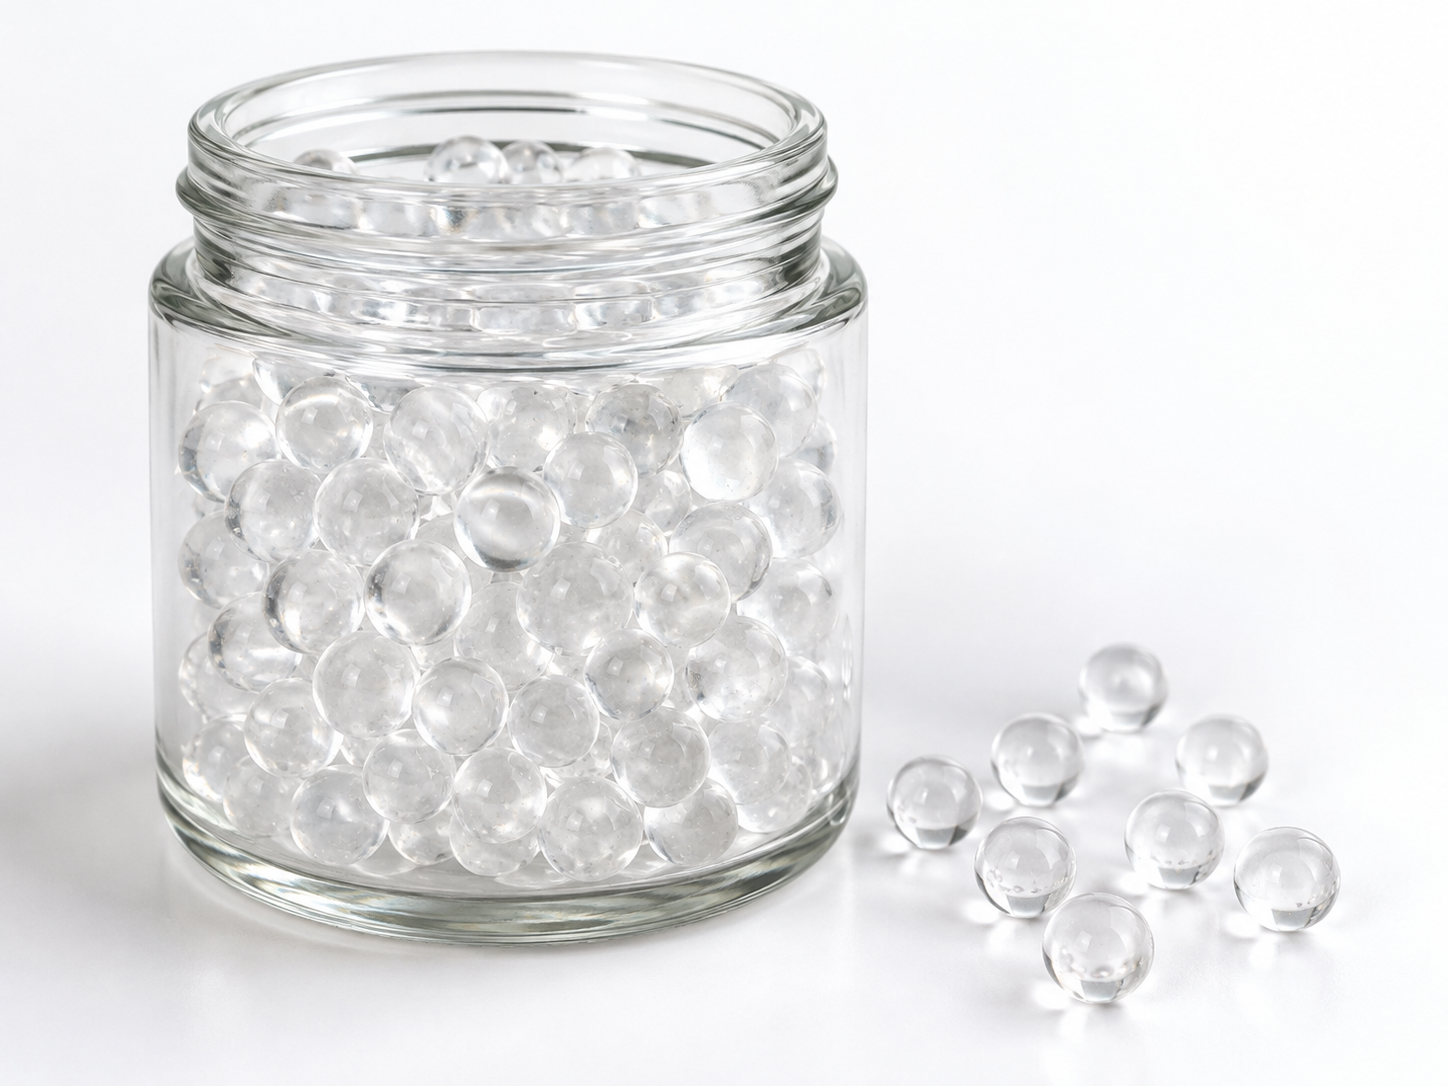
Understanding Why Polyphosphate Media Breaks in Automated Systems
The single most effective way to limit polyphosphate ball damage during automated filling is to control the kinetic energy transferred to the media at every point of contact—by reducing drop height, moderating fill velocity, using cushioned transfer zones, and selecting media with adequate mechanical resilience for the specific handling system. Damage is rarely caused by one factor alone; it results from the cumulative effect of impact, compression, and vibration that occurs as beads move from storage hopper through chutes, tubes, and into filter housings or bags.
Operators who run semi-automatic or fully automatic filling lines for scale-inhibition cartridges, point-of-use canisters, or industrial dosing vessels often report a yield loss between five and twenty percent per batch. Most of that loss is not product defect—it is handling damage. Understanding the failure modes helps you design around them.
How Polyphosphate Balls Fail Under Mechanical Stress
Polyphosphate media, whether supplied as siliphos crystal, granular polyphosphate, or spherical sequestrant beads, is a glassy or semi-crystalline solid. It inhibits scale by forming a thin protective film on pipe and appliance surfaces, a function sometimes confused with water softening. It does not remove existing scale, nor does it soften water in the ion-exchange sense. Its primary job is threshold treatment: keeping calcium carbonate and other hardness salts in solution long enough to pass through a system without depositing.
That chemical function has nothing to do with mechanical strength, but the physical form of the media matters enormously in an automated fill environment. Beads typically range from one to several millimetres in diameter. Their fracture toughness is lower than that of ceramic or polymer filter media. When a bead strikes a hard surface at speed, it chips or shatters. When beads are compressed between a filler plate and a pile of already-loaded media, they crack under point loads. Repeated low-level vibration during transport on conveyors or vibratory feeders creates micro-fractures that weaken beads until they break on the next impact.
Three damage categories dominate in automated filling:
- Impact fracture: free-fall or high-velocity discharge from a hopper onto a hard surface
- Compression cracking: beads caught between the filler nozzle, a weight plate, or already-settled media
- Attrition wear: bead-on-bead grinding during vibratory feeding, pneumatic conveying, or turbulent flow through chutes
Practical Steps to Reduce Damage at Each Stage
1. Hopper Design and Discharge Control
The hopper is where most damage begins. A steep-walled hopper with a large orifice creates a high-velocity slug of media that impacts the receiving surface. Replace it with a shallow-angle, mass-flow hopper that feeds a controlled, narrow stream.
Use a rotary valve or a slow-opening gate rather than a simple slide gate. Target a discharge velocity low enough that beads arrive at the filling point with minimal kinetic energy—generally under one metre per second for standard polyphosphate spheres, though the exact threshold depends on bead size and density. If your line currently uses a gravity drop greater than thirty centimetres, installing a short transfer chute with a flexible or rubber-lined interior can cut impact energy by half or more.
2. Transfer Chutes and Tubes
Every bend, every diameter change, every place where the media stream hits a wall is a risk point. Use smooth-bore tubing with a diameter at least three times the median bead size. Avoid ninety-degree elbows; use long-radius bends instead. Where direction changes are unavoidable, line the impact zone with polyurethane or silicone to absorb energy without introducing contaminant dust.
If you use pneumatic conveying, keep air velocity low. High-velocity air streams not only erode beads but also create turbulent collisions inside the line. A dilute-phase system at reduced pressure often outperforms a dense-phase push for fragile media.
3. The Filling Nozzle and Fill Zone
This is the stage where compression damage is most likely. As the vessel or cartridge fills, the rising bead pile presses upward against the nozzle or filler plate. If the nozzle is rigid and the fill continues without relief, beads at the bottom fracture.
Solutions include:
- A spring-loaded or floating filler plate that rises with the media level
- A side-fill or bottom-fill design that avoids direct downward pressure on settled beads
- A fill-level sensor that stops the feed before the pile reaches the nozzle
For bag-filling operations, consider a pre-formed soft inner bag that cushions the media as it enters the outer packaging. This is especially relevant for smaller polyphosphate products destined for point-of-use cartridges.
4. Vibration Management
Vibratory feeders are common in automated lines because they handle small parts reliably. For polyphosphate media, however, continuous vibration fatigues beads. If you must use vibration, limit it to the feeding stage only—turn it off once beads enter the fill chute. Use low-amplitude settings and isolate the feeder from the fill station with a rubber mount or flexible coupling.
Media Selection Factors That Affect Damage Resistance
Not all polyphosphate media behaves the same under stress. Differences in manufacturing process, binder content, firing temperature, and bead geometry all influence how much abuse a product can tolerate.
| Property | Effect on Handling Durability | What to Confirm |
|---|---|---|
| Bead hardness and fracture toughness | Higher toughness resists impact and compression | Request mechanical test data from the supplier for the specific grade |
| Bead size distribution | Uniform, larger beads generally survive handling better than fine, irregular particles | Verify the mesh or sieve range matches your application and equipment tolerances |
| Surface coating or binder | Some coatings add slight cushioning; others make beads more brittle | Ask whether the product uses a binding agent and how it affects physical strength |
| Moisture content | Dry beads are more brittle; slightly higher moisture can reduce static and chip propagation but may affect shelf life | Confirm storage and handling humidity requirements |
When sourcing polyphosphate media for an automated line, do not assume that a product marketed for water treatment will automatically survive industrial filling equipment. Ask the supplier for information on mechanical durability under the specific conditions your line creates.
Common Mistakes That Increase Breakage
- Running the line too fast. Throughput pressure leads operators to open gates fully and skip cushioning steps. The yield loss from extra breakage usually exceeds the time saved.
- Using the same fill setup for different media. A line tuned for dense ceramic media will destroy lightweight polyphosphate beads. Each media type needs its own calibrated settings.
- Ignoring static charge. Polyphosphate beads can accumulate static, causing them to cling to chutes and drop in clumps rather than a smooth stream. Clump impacts create concentrated force points. Ground your equipment and consider mild anti-static measures if the problem is recurring.
- Over-filling. Topping off a vessel after the main fill adds unnecessary compression cycles on already-settled media.
When to Evaluate a Different Media Form
If, after optimizing your line, breakage rates remain unacceptably high, consider whether a different physical form of polyphosphate might suit your application. Some suppliers offer block or tablet forms that are less prone to impact damage during handling, though they may require different dissolution or dosing arrangements. Granular forms with a broader size range can sometimes pack more densely without the same fracture risk, but they may not fit every cartridge or dosing device.
Any change in form must be evaluated against the actual performance requirement—sequestration capacity, dissolution rate, compatibility with the water chemistry in your system, and regulatory suitability for the intended use. A form that handles better but underperforms chemically is not a solution.
Questions to Ask Before Finalizing Your Setup
Before committing to a media grade and a filling configuration, confirm the following:
- What is the median bead size and size distribution of the polyphosphate product you plan to use?
- What is the maximum drop height and fill velocity your current equipment generates?
- Does the media supplier provide mechanical durability data relevant to your handling method?
- What is the acceptable breakage or fines percentage for your end product or application?
- Are there regulatory or certification requirements for the media in your destination market, particularly if the application involves potable water?
The last point deserves emphasis: suitability for drinking-water contact must be verified for the exact product, under the specific use conditions and in the jurisdiction where it will be sold or installed. A general description of material grade is not a substitute for a documented compliance assessment.
Working with a Supplier Who Understands the Full Picture
Damage during automated filling is as much a materials-handling problem as it is a product-quality problem. The most productive conversations with a polyphosphate supplier happen when you bring both sides of the equation: your equipment realities and your performance targets. ENVO CHEMICAL supplies polyphosphate media for a range of water-treatment applications and can discuss product characteristics that matter for automated processing—including bead form, size range, and handling guidance—when you share details about your system.
If you are setting up or optimizing an automated fill line for polyphosphate media, send us your application type, source-water conditions, equipment configuration, target fill volume, and the media specification you are evaluating. We will help you match the right product to your process.
