
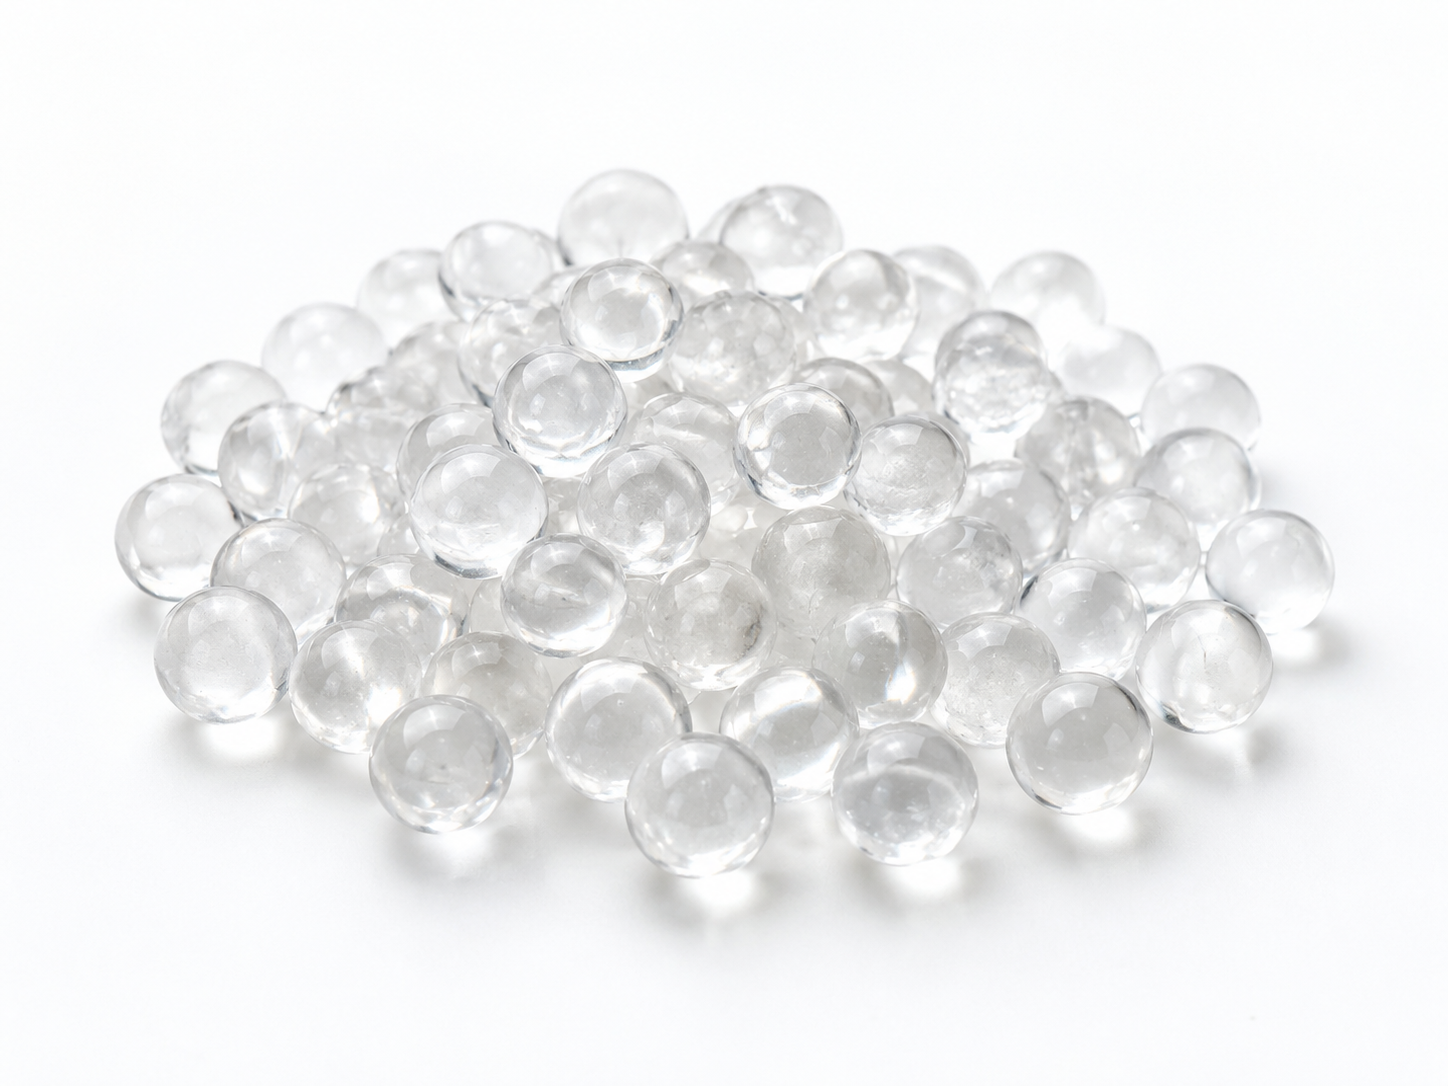
What “production yield” actually means for polyphosphate crystal balls
Polyphosphate production yield is best managed as a three-way mass balance: every kilogram leaving the line is either a saleable ball, a fine, or a reject. Yield is not a single fixed number, because it moves the moment you change where the cut points sit. A plant that sets a tight size window will call more material “fine” than a plant that accepts a wider band, even when both run the same process. That is why two suppliers can quote very different yield figures for what looks like the same product.
The practical goal is not to maximize one number on a dashboard. It is to ship a product with a predictable size distribution and dissolution behaviour, while keeping the value locked inside the fines and rejects recoverable instead of writing it off as waste.
A terminology note before going further: products sold as siliphos crystal, phosphate crystal, and polyphosphate media are often grouped together commercially, but they are not automatically interchangeable. Phosphate glass composition, forming method, size grading, and regulatory status vary by manufacturer, and specifications should be matched to the actual product rather than to the category name.
Defining the three output streams
Saleable balls
A saleable ball is one that satisfies every characteristic in the released specification, not just diameter. In practice the acceptance criteria usually cover:
- Size: nominal diameter inside the agreed tolerance band, established by screening.
- Shape: acceptably spherical, without flats, twins, tails, or heavy deformation.
- Integrity: no visible cracks, chips, or internal fractures that would promote breakage in handling.
- Appearance: colour and translucency consistent within the batch, free from dark specks or discoloured zones.
- Cleanliness: no metal fragments, packaging fibre, or cross-contamination from other products.
- Chemistry and moisture: conforming to the batch specification and to whatever moisture limit applies to the product.
Numeric limits for each of these belong in the product specification and should be confirmed with the customer or the internal quality function. They are product-specific and should not be assumed from this general list.
Fines
Fines are particles below the lower cut of the saleable window, plus the dust fraction generated by abrasion. In many polyphosphate processes the fines are chemically close to the saleable balls, because both come from the same melt or the same forming step. That chemical similarity is what makes them worth recovering rather than discarding.
Fines are also the stream most likely to be underestimated. Dust sticks to equipment, travels with air, and settles into cartons, so the true fine generation rate is only visible if dust collection and floor sweepings are weighed and counted rather than ignored.
Rejects
Rejects are out-of-specification for reasons other than simple undersize. Typical causes include agglomerated clusters, elongated or malformed pieces, cracked or crumbled balls, discoloured material, moisture-damaged product, and anything contaminated by foreign matter.
The important distinction is that a reject is defined by the cause, because the cause determines whether the material can be recycled. A cracked ball made from compliant chemistry may be perfectly recyclable through a re-melt route. A ball contaminated with metal dust or degraded packaging is not.
| Stream | Usual origin | Preferred disposition | Main risk if mishandled |
|---|---|---|---|
| Saleable balls | In-spec forming and cooling output | Pack and release | Dust carry-over from upstream screening |
| Fines | Breakage, tumbling, transfer points, screening | Verified internal recycle, or sale to an application that accepts a finer grade | Moisture pickup, caking, contamination, dust exposure |
| Rejects (clean) | Shape, cracks, colour, agglomerates | Re-melt or reprocess after verification | Impurity accumulation across repeated cycles |
| Rejects (contaminated) | Foreign matter, degraded packaging, unknown history | Segregate and dispose according to local rules | Contaminating a whole recycled batch |
A practical classification workflow
Separating the streams reliably is a sequence, not a single screening step. Skipping a step usually shows up later as customer complaints about dust or inconsistent dissolution.
- Fix the specification before the run. Agree the upper and lower size cuts, the shape criteria, the colour standard, and the moisture limit. A cut point chosen after screening is not a specification, it is a rationalization.
- Screen in stages. Use a first deck to remove oversize and agglomerates, a main deck that defines the saleable window, and a fine deck to split usable fines from dust. Multi-stage screening reduces blinding and improves separation efficiency compared with a single crowded deck.
- Inspect the saleable cut. Visual inspection, manual or automated, removes cracked, discoloured, and malformed pieces that passed the size test. This is the step where “size-passing” is converted into genuinely saleable product.
- Weigh every stream. Record the mass of saleable balls, each fines fraction, clean rejects, and contaminated rejects. Include dust collected by extraction systems.
- Close the mass balance. Input mass should reconcile with output mass plus accounted losses within a stated tolerance. An unexplained gap usually means dust is escaping or material is being double counted after recycling.
- Route each stream deliberately. Assign a destination and a verification requirement to each one. “Put it back in” is not a routing decision.
- Record and trend. Track the split by batch and by shift, so a drift in fine generation is visible before it becomes a yield crisis.
Choosing the cut points
Cut points should be driven by the end application, not by convenience. Polyphosphate crystal media is used for scale inhibition in water systems, and in some formulations for corrosion inhibition as well. It does not soften water in the ion-exchange sense, does not filter particulates, and does not disinfect. Its behaviour depends on controlled dissolution, and dissolution depends strongly on particle size.
Smaller particles have a higher surface-area-to-volume ratio and therefore release polyphosphate faster than large ones. If fines are allowed to remain in a cartridge or a dosing device, the initial release rate can be higher than intended, the media bed can compact or cake, and the effective service interval can shift. In drip irrigation and other small-orifice systems, dust can also contribute to clogging.
That is the technical reason a coarse cut exists at all. The right aperture is the one that produces the dissolution profile and hydraulic behaviour the equipment was designed around, which is why it should be confirmed with the device manufacturer or the end user rather than copied from a different application.
Measuring yield correctly
Two figures are worth reporting separately, because they answer different questions.
First-pass yield counts only material that came off the line saleable on the first attempt:
First-pass yield (%) = saleable mass ÷ (saleable + fines + clean rejects + contaminated rejects) × 100
Recovered yield adds the fines and clean rejects that were successfully recycled and eventually shipped as saleable product. Recovered yield tells you how well the recovery loop works; first-pass yield tells you how well the forming process works. Reporting only the combined figure hides the difference.
Two measurement cautions are commonly overlooked. First, if you correct for moisture, state the basis, otherwise your yield will drift as ambient humidity changes. Second, material that is recycled internally must not be counted twice: it enters the balance once as a fine or reject and again only when it leaves as saleable product.
Reducing fine generation at the source
Once the split is measured, the highest-value improvement is usually upstream of the screen. Areas worth reviewing include transfer points and drop heights, the cooling and solidification stage where thermal stress can initiate cracks, tumbling or forming parameters, screening deck loading and screen condition, dust extraction effectiveness, and the packaging step where abrasion continues to generate dust. Each of these should be evaluated against the actual process data rather than adjusted on assumption.
Recycling fines and rejects: conditions and limits
Recycling looks straightforward and rarely is. Clean fines and clean rejects can often be returned to the process, but only when several conditions hold:
- The chemistry of the recycled stream is verified, not assumed.
- Contamination status is known, including handling history.
- The recycling route is defined: direct re-melt, re-forming, or another validated method.
- The effect on colour, dissolution rate, and final size distribution is checked against specification.
- Records allow the recycled content to be traced in the finished batch.
The main long-term risk is accumulation. Impurities that are negligible in a single pass can concentrate over repeated cycles and shift the product’s appearance or dissolution behaviour. This is why a recycle rate that works for a few batches may eventually require a purge stream.
There is also a market question. Fines are not automatically a lower grade of the same product, and material that has been exposed to uncontrolled humidity or handling may no longer meet the original specification. If fines are sold separately, they need their own specification and their own stated application limits.
What buyers should ask a supplier
For importers, distributors, filter manufacturers, and equipment builders, the yield discussion matters because it explains what is actually inside the carton. Useful questions include:
- What is the declared size distribution, and how is it measured?
- Is there a maximum fines or dust content, and how is it verified at dispatch?
- What defines a reject, and what happens to recycled material?
- Is moisture content specified, and on what basis?
- For drinking-water applications, what documentation supports the exact product for the exact market? Food-grade status alone does not establish drinking-water suitability.
In some markets, drinking-water treatment chemicals are assessed under recognised schemes such as NSF/ANSI/CAN 60, but the applicable requirement depends on the destination country and the specific product. This must be confirmed per product and per market rather than inferred from a general grade description.
Frequently asked questions
Does polyphosphate crystal media soften water?
No, not in the ion-exchange sense. It does not remove calcium and magnesium from the water. It is used for scale inhibition, and in some formulations for corrosion inhibition, by interfering with scale formation and by forming a thin protective film on metal surfaces. Softening, filtration, and disinfection are separate functions performed by different technologies.
Can fines be sold as the same product?
Only if they meet a specification that the customer has accepted. Fines dissolve faster than full-size balls because of their higher surface-to-volume ratio, so they change the release profile of a device. Where fines are offered commercially, they are normally sold against a separate specification and a defined application.
What is a typical yield percentage?
There is no defensible universal figure. Yield depends on the forming route, the size window, the recycling policy, and how dust losses are accounted for. Anyone quoting a number without stating those conditions is quoting an assumption. The useful comparison is a plant’s own yield trend over time under a fixed specification.
Is a food-grade declaration the same as drinking-water approval?
No. Food-grade status addresses one set of requirements; drinking-water suitability depends on the exact product, the dose, the contact conditions, and the regulations of the destination market. The two must be verified separately.
Discuss your grading or sourcing requirement
If you are setting up classification for a polyphosphate line, or sourcing polyphosphate crystal media and need clarity on size distribution, fines limits, moisture specification, and documentation for your market, ENVO CHEMICAL can review the requirement with you. It helps to include your application or device type, the target size range, source-water conditions where relevant, the required specification and documentation, quantity, and destination market. With those details, the discussion can start from your actual constraints rather than a generic product list.
