
Does Cartridge Welding Heat Damage Polyphosphate Media?
The short answer is yes — excessive or uncontrolled heat during cartridge end-cap welding can degrade polyphosphate media, reducing its ability to sequester hardness ions and inhibit scale formation. However, the degree of damage depends on the welding method, temperature profile, dwell time, and the specific formulation of the polyphosphate blend. When manufacturers understand these variables, they can design sealing processes that preserve media performance without sacrificing cartridge integrity.
This article examines what happens to polyphosphate crystal media when it is exposed to the heat of cartridge welding, why the risk matters for water-treatment applications, and what process controls help filter and equipment manufacturers protect product quality.
Why Heat Exposure Matters for Polyphosphate in Sealed Cartridges
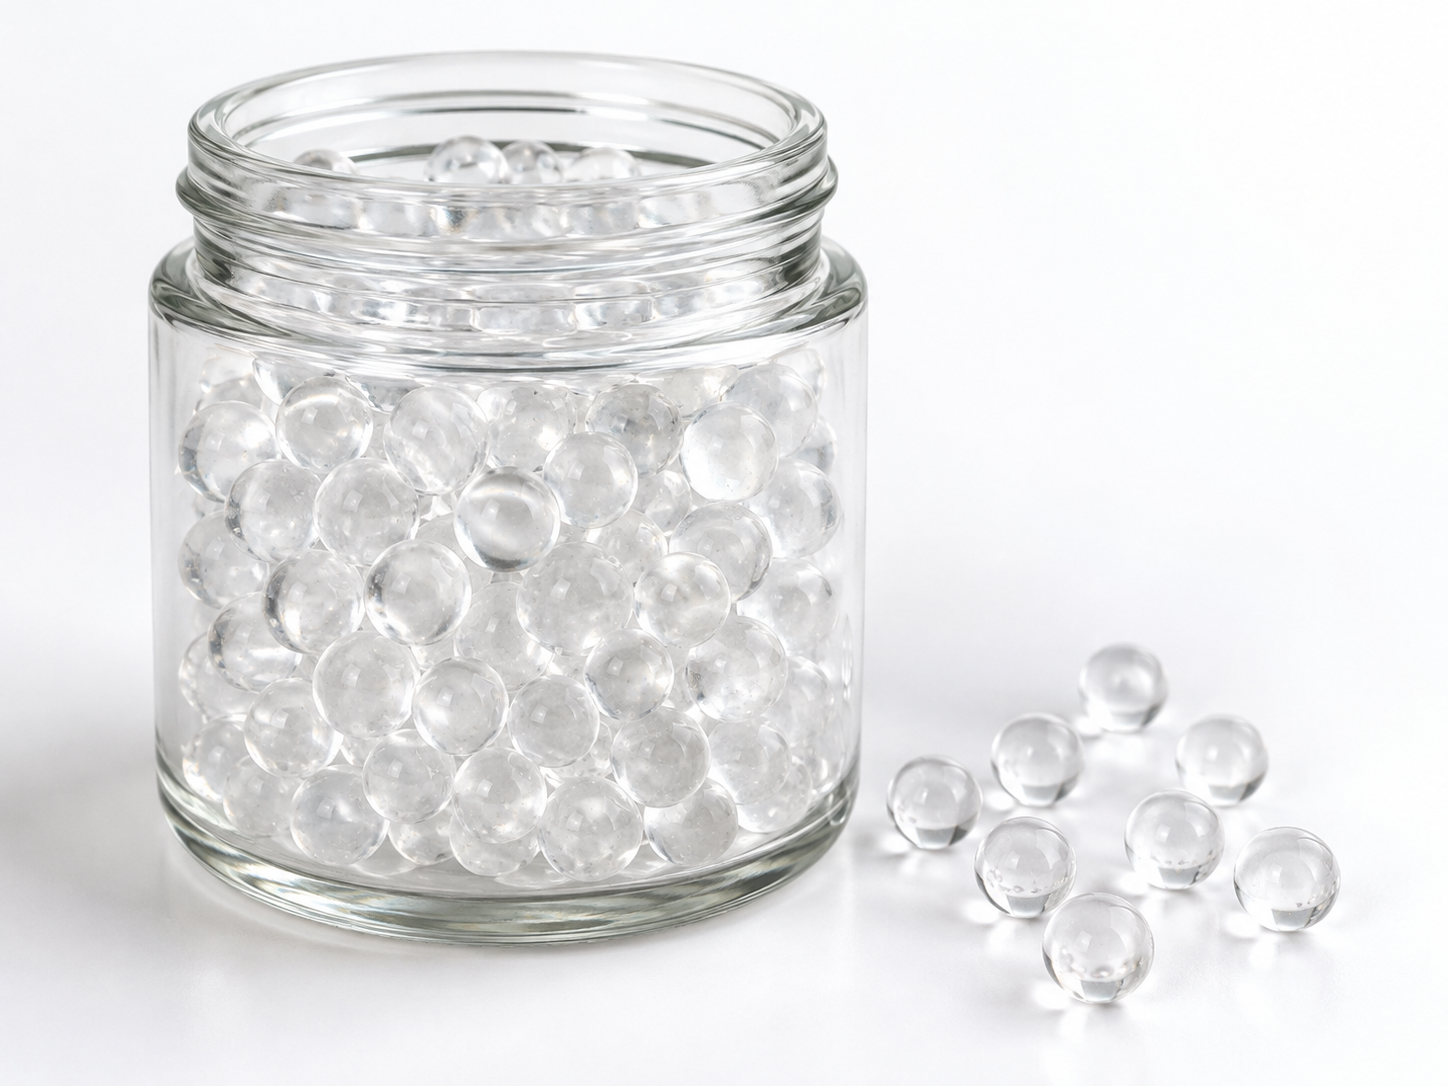
Polyphosphate media — typically supplied as glass-like beads or crystals composed of long-chain phosphate polymers — works by slowly dissolving into water and binding with calcium, magnesium, and other metal ions. This sequestration prevents those ions from precipitating as scale on pipes, heating elements, and appliances. The mechanism relies on the integrity of the polymer chains.
When a polyphosphate cartridge undergoes end-cap welding, the heat must pass through the cap and, to some extent, into the media bed near the seal. If local temperatures climb too high or hold too long, several things can occur:
- Partial depolymerisation: Long phosphate chains break into shorter fragments that have weaker sequestration capacity.
- Premature dissolution or fusion: Crystal surfaces may soften or partially melt, causing beads to stick together and reducing the effective surface area available for controlled release.
- Color change: Overheated polyphosphate often shifts from a clear or slightly amber appearance to a milky or opaque state, a visible indicator that the crystal structure has been altered.
None of these changes immediately destroy the media, but they shorten the functional lifespan of the cartridge and can cause inconsistent dosing of phosphate into the treated water stream. For end users relying on predictable scale inhibition, this inconsistency is a real operational problem.
Welding Methods and Their Thermal Profiles
Not all cartridge-sealing techniques apply heat in the same way. Understanding the difference helps manufacturers choose a method that minimises media exposure.
Ultrasonic Welding
Ultrasonic welding uses high-frequency vibration to generate localised heat at the joint between the cap and the cartridge body. The advantage is that heat is concentrated at the seam rather than conducted broadly through the media. Cycle times are short — typically under one second — which limits the thermal window. For polyphosphate cartridges, ultrasonic welding is generally the least risky method, provided the amplitude and pressure settings are calibrated so that vibration energy does not propagate deeply into the bead bed.
Hot-Plate or Heat-Seal Welding
In hot-plate welding, a heated element contacts the cap and the cartridge end simultaneously, melting the plastic to form a bond. This method exposes a larger area to elevated temperatures for a longer duration. If the plate temperature is set too high or the dwell time is extended to compensate for poor fit-up, heat can travel several centimetres into the media. Manufacturers using this method should verify that the temperature at the media surface stays well below the softening point of the polyphosphate crystals.
Spin Welding and Infrared Methods
Spin welding relies on friction-generated heat and is more common with larger housings. Infrared sealing uses radiant energy. Both can be adapted for cartridge work, but each introduces a different heat distribution pattern. The key principle remains the same: the thermal energy reaching the media must be controlled, measured, and kept within safe limits.
| Welding Method | Typical Heat Source Location | Risk to Polyphosphate Media | Best-Practice Control |
|---|---|---|---|
| Ultrasonic | Seam interface, vibration-generated | Low to moderate | Calibrate amplitude; limit weld time |
| Hot-plate / heat seal | External plate contact | Moderate to high | Monitor plate temperature; reduce dwell time |
| Spin welding | Friction at rotating joint | Variable | Control rotational speed and pressure |
| Infrared | Radiant energy through cap | Moderate | Shield media bed; use pulsed energy |
Practical Steps to Protect Media During Welding
Filter manufacturers and equipment assemblers can adopt several measures to keep polyphosphate media within its functional range during the sealing process.
- Leave a buffer zone. Do not fill the cartridge completely to the cap. A gap of at least 10–15 mm between the top of the media bed and the sealing surface reduces direct heat conduction.
- Use a thermal barrier if possible. Some manufacturers place a thin disc of inert material — such as a polypropylene spacer — between the media and the cap. This absorbs some heat without contaminating the water stream.
- Validate with temperature logging. Place a thermocouple or infrared sensor at the media surface during test welds. Record the peak temperature and the time above any threshold you define as safe. Repeat across multiple units to account for variation.
- Perform post-weld performance checks. Run a short dissolution or sequestration test on welded cartridges and compare results against unwelded control samples. If phosphate release rates or hardness-binding capacity drop noticeably, adjust the welding parameters.
- Document the process window. Define acceptable ranges for temperature, time, and pressure specific to the polyphosphate formulation you are using. Different phosphate blends have different thermal sensitivities, so generic settings are not reliable.
These steps do not eliminate risk entirely, but they create a repeatable process that gives confidence the media will perform as expected once installed in the field.
Polyphosphate Media: What It Does and What It Does Not Do
A common source of confusion in water treatment is the overlap between terms like scale inhibition, water softening, scale removal, and corrosion inhibition. Polyphosphate media is primarily a scale inhibitor and a corrosion inhibitor. It does not soften water in the ion-exchange sense, nor does it remove existing scale. It does not filter particles, and it is not a disinfectant.
Specifically, polyphosphate works by:
- Binding free calcium and magnesium ions so they remain in solution rather than forming deposits.
- Forming a thin protective film on metal surfaces that slows corrosion.
- Releasing phosphate gradually as the crystals dissolve, providing a timed-release effect that extends cartridge life.
If the welding process damages the crystal structure, the release profile changes. Instead of a steady, predictable dose, the media may dump phosphate quickly at first and then taper off, or it may under-dose from the start. Either outcome defeats the purpose of using a metered polyphosphate cartridge.
When to Reassess Your Welding Process
You should review your cartridge-sealing procedure if any of the following occur:
- Finished cartridges show visible cloudiness, fusing, or discolouration near the sealed end.
- Batch-to-batch performance tests show wider variation than expected.
- You switch to a new polyphosphate supplier or a different crystal grade.
- You change the cartridge housing material, cap design, or welding equipment.
- Customer complaints reference inconsistent water quality or shortened cartridge life.
Each of these signals suggests that the thermal conditions at the media may have shifted, and a fresh validation cycle is warranted before continuing production.
Selecting the Right Polyphosphate Formulation for Welded Cartridges
Not all polyphosphate media behaves identically under heat. Some formulations are engineered with higher thermal stability, using modified phosphate chains or blended compositions that resist depolymerisation at elevated temperatures. When specifying media for a cartridge that will be welded, ask your supplier about:
- The maximum short-term temperature the crystals can tolerate without measurable loss of sequestration capacity.
- Whether the product has been tested in conditions that simulate welding heat exposure.
- The recommended filling density and buffer zone for sealed cartridge applications.
- Any compatibility notes with common cartridge-housing polymers such as polypropylene or polycarbonate.
ENVO CHEMICAL supplies polyphosphate crystal media for water-treatment cartridges and can provide formulation-specific guidance on thermal exposure limits when requested. If your production line uses a particular welding method, sharing those parameters helps the supplier confirm suitability.
Frequently Asked Questions
Can polyphosphate media recover its performance after being overheated during welding?
No. Once the phosphate chains are broken or the crystal structure is fused, the change is permanent. The media cannot be “re-activated” by soaking or rinsing. Prevention through process control is the only reliable approach.
Is there a universal safe temperature for welding polyphosphate cartridges?
No single temperature applies to every product. The safe limit depends on the specific phosphate blend, bead size, and exposure time. Manufacturers must determine the threshold for their own material through testing rather than relying on a general figure.
Does the color of the media after welding indicate damage?
A color shift toward cloudiness or white opacity is a strong visual clue that the crystals have been thermally affected. Clear or lightly amber beads are generally a good sign. However, some damage may occur without obvious color change, so visual inspection alone is not sufficient.
Should I test every welded cartridge individually?
Individual testing of every unit is usually impractical. Instead, validate the welding process with a statistical sample plan — test a representative number of cartridges from each production batch and confirm they meet release-rate and sequestration benchmarks.
Does this concern apply to all phosphate-based media, including orthophosphate blends?
The thermal sensitivity described here is most relevant to long-chain polyphosphate. Orthophosphate or blended formulations may behave differently. Always confirm the thermal behaviour of the exact media you intend to use.
Get Specific Guidance for Your Application
If you manufacture or assemble polyphosphate cartridges and need to confirm whether your current welding process is compatible with a particular media grade, share the following details: your cartridge housing material, the welding method and approximate settings, the media formulation or grade you are using or considering, and the water-treatment application the cartridge will serve. ENVO CHEMICAL can then help you evaluate the fit and flag any process adjustments that may be needed.
