
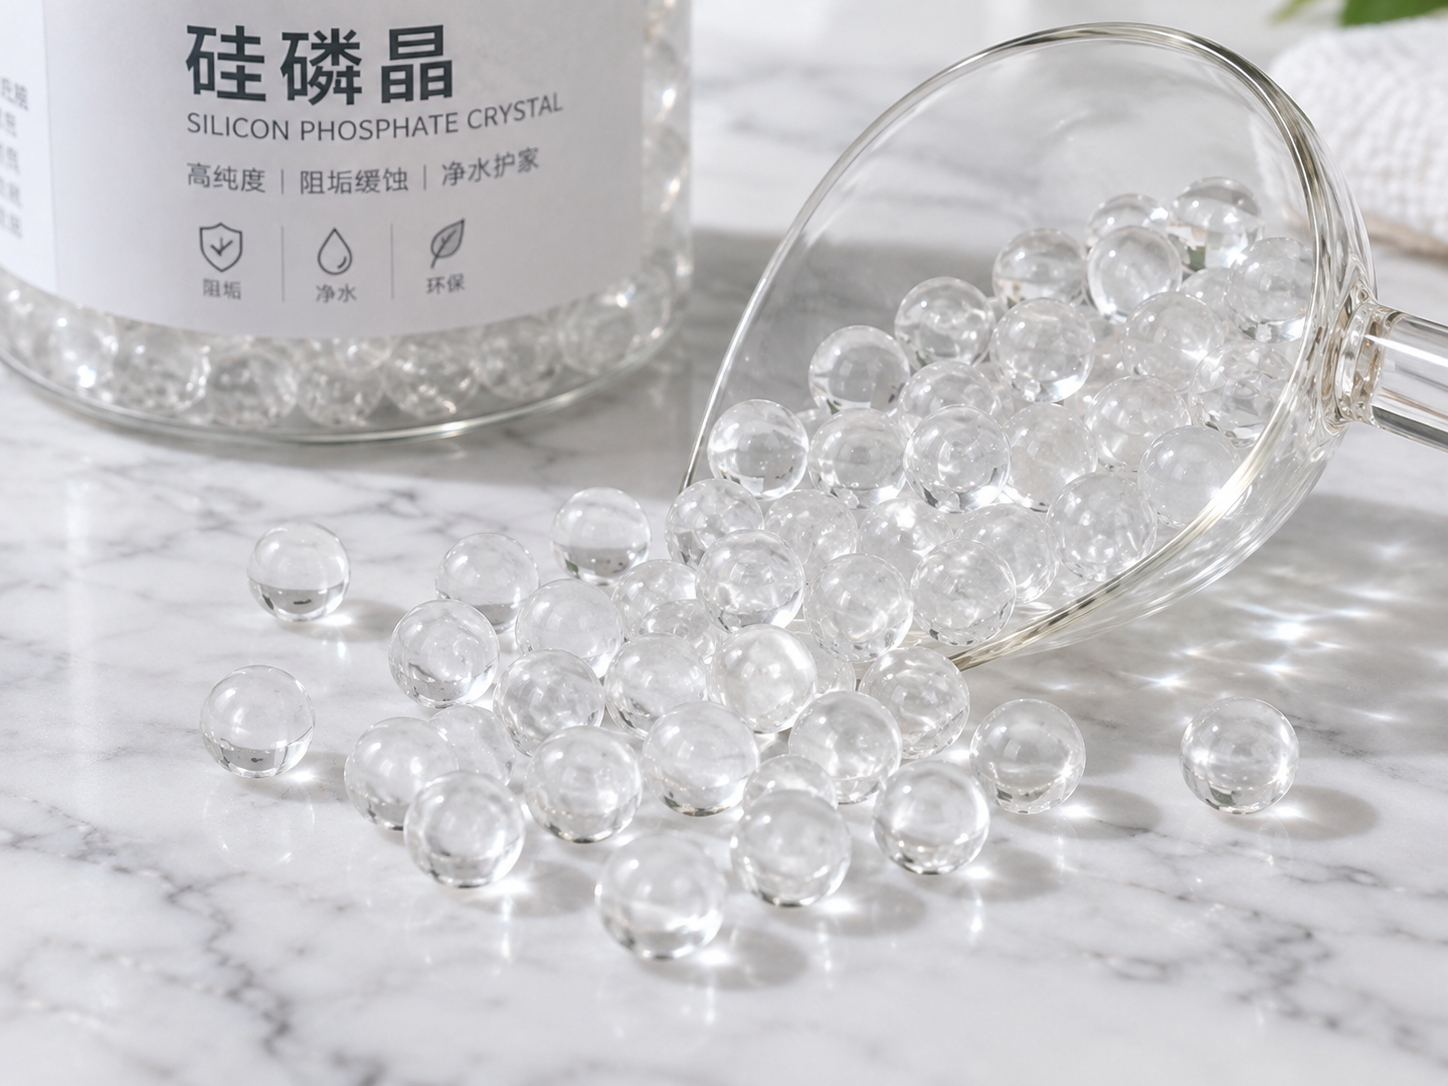
Verifying polyphosphate media restraint at very low fill levels is not a single inspection. It is a short, three-part check: confirm that the retention geometry actually blocks the smallest particle in the media batch, confirm by mass balance and downstream particle capture that nothing escapes the housing under realistic flow and handling conditions, and confirm by post-test teardown that the bed has not migrated, channelled, or deformed the retainer. At low fill, no one of these checks substitutes for the others, because the assumption that normally makes restraint easy — a deep bed that supports itself and preloads the upper retainer — no longer applies.
This matters most to cartridge and filter-housing manufacturers, OEM assemblers, water-treatment equipment builders, and importers who approve a media specification before it ships. If you are the person signing off on a low-fill cartridge design, the sections below are written for your bench, not for a catalogue.
Why a low fill level changes the whole verification logic
In a conventionally filled housing, the polyphosphate crystal bed sits deep enough to press against the upper retention pad or screen. That contact does three jobs: it keeps the retainer seated, it limits particle movement, and it forces flow through the bed rather than over it. Reduce the fill level and all three weaken at once. Headspace appears, the bed can tumble under flow, and a retainer held only by bed pressure may lift or shift.
Low fill is also a moving target. Polyphosphate media dissolves in service, so the bed gets shallower over time. A cartridge that passes restraint checks on day one may behave differently once the inventory has been consumed down to a fraction of the original charge. Verification should therefore be run at the minimum fill level you intend to allow, not at a comfortable nominal level.
Fix the vocabulary before testing
Restraint, retention, containment, and fixation are often used interchangeably in media specifications, which causes test plans to miss the real risk. For clarity:
- Restraint — keeping the media body in its intended position inside the housing.
- Retention — preventing individual particles from leaving through the outlet.
- Containment — preventing media from entering any path other than the intended flow path, including bypass channels and dead zones.
- Performance — whether the media still does its job of inhibiting scale in the treated water. This is a separate question from restraint and needs its own evidence.
Note also that polyphosphate media is not a single standardized material. Trade names such as Siliphos are brand names, and products sold as “phosphate crystal,” “polyphosphate crystal,” or “siliphos-type” media can differ in particle-size distribution, dissolution behaviour, and approved applications. If you are verifying restraint, this matters: your retention element has to match the actual particle-size distribution of the actual batch you are running.
Layer 1: Geometry and particle-size verification
The smallest particle decides the aperture
A retention screen only works if its apertures are smaller than the smallest particle likely to reach it. Obtain the supplier’s particle-size distribution, or sieve a representative sample yourself, and compare the lower end of that distribution with the aperture of every downstream retention element — outlet mesh, slotted screen, sintered disc, or non-woven pad. If the media is shipped with fines, or if crystals can fracture during assembly and shipping, the fines are the fraction that will find a way out.
Check the seal, not just the screen
Most media escape in low-fill cartridges happens around the edge of the retainer, not through the mesh. Verify that the retention element seals against the housing wall or the end cap, and that the seal does not depend on the bed pushing it into place. If the design relies on a spring, a foam compression pad, or bed pressure to keep the retainer seated, test that retainer with the media charge removed entirely. If it can lift or shift when empty, it will eventually do so in service.
Layer 2: Mass balance and downstream particle capture
Separate escape from dissolution
A simple before-and-after weight check is a common first instinct, and at low fill levels it is easy to misread. Polyphosphate media loses mass by dissolving, which is the intended mechanism, so total mass loss cannot be attributed to escape. Use two independent measurements instead:
- Capture everything leaving the outlet on a fine filter or mesh rated below the smallest particle size, then weigh and inspect the captured solids. Phosphate crystals can be distinguished from unrelated debris by appearance and by a simple phosphate identification test.
- Measure dissolved phosphate in the effluent separately, so dissolution is accounted for rather than mistaken for particle loss.
Choose a test duration and condition set in which the expected dissolution loss is small compared with the detection threshold of your weighing method. If you cannot achieve that, extend the downstream capture approach rather than relying on total mass loss.
Run it at the real fill level and orientation
Assemble the test cartridge at the minimum allowed fill, in the orientation it will see in service, and run it at the flow rate and pressure the equipment will actually deliver — including any surge or start-stop behaviour. A horizontal or inverted installation can change where crystals settle and which retention surface they contact.
Layer 3: Flow, fluidization, and bypass observation
A transparent test housing is the cheapest restraint diagnostic available. Build one version of the cartridge with a clear body and observe the bed at the highest intended flow rate. What you are looking for:
- Whether crystals lift, circulate, or tumble instead of staying settled.
- Whether a clear channel forms above or beside the bed, letting water pass without contacting the media.
- Whether the bed shifts as a mass toward one end of the housing, loading a single retention surface.
- Whether the upper retainer moves, tilts, or loses contact with the housing wall.
Remember that a bypass channel is a containment failure even when no particle leaves the housing. Restraint and treatment performance are related but distinct: media held perfectly in place but bypassed by flow delivers no benefit. If dye tracing or a conductivity tracer shows flow reaching the outlet without passing through the bed, address the fill level or the internal flow path before signing off on the design.
Handling and transport verification
Low-fill cartridges are more sensitive to shipping vibration than full ones, because there is room for the media to move. A vibration-table run or a controlled drop test followed by teardown will reveal migration, fine generation, retainer displacement, and crystals embedded in or abrading against the mesh. If you cannot run a full transport simulation, at minimum shake the assembled unit by hand in each axis and inspect the outlet side of the retainer for crystals.
A compact verification table
| Check | What it establishes | What it does not establish |
|---|---|---|
| Sieve data versus aperture size | Whether the retention element can physically block the smallest particles | Whether the element stays seated in service |
| Seal and preload inspection with the media removed | Whether retention depends on bed pressure | Whether the seal survives vibration and thermal cycling |
| Downstream particle capture plus dissolved-phosphate measurement | Whether particles actually leave the housing, separated from dissolution | Where inside the housing the escape path is located |
| Transparent-housing flow observation | Bed movement, channelling, and bypass behaviour | Long-term behaviour as the bed dissolves down |
| Vibration or drop test with teardown | Migration and damage caused by handling and transport | In-service flow effects |
Typical low-fill failure modes to look for
- Fines passing through a mesh that is adequate for whole crystals.
- Media escaping around an unsealed retainer edge.
- An upper retainer that was held only by bed pressure and now floats free.
- Bed fluidization at high flow, producing abrasion and additional fines.
- Flow channelling over the top of a shallow bed, reducing contact time.
- Bed consolidation at one end of the housing, leaving a large empty flow area.
- Cartridges that pass on day one but fail after the bed has dissolved to its minimum practical depth.
What to record, and where acceptance limits come from
Document the fill level in more than one form, because “low fill” is ambiguous. Record the dry media mass charged, the settled bed height before and after wetting, and the measurement method used, since dry and wet settled heights differ. Record the particle-size distribution of the batch, the aperture of each retention element, the flow rate and orientation used for testing, and the mass of solids captured downstream.
Acceptance limits — how much captured solids is tolerable, how much bed movement is acceptable — should come from your own validated design standard, the housing or cartridge specification, or documented supplier guidance. Do not adopt numbers from an unrelated product or assume that a value published for a different housing applies to yours. If no verified limit exists, state that the limit must be established for the specific design before production release.
What to confirm with the media or cartridge supplier
Before finalizing a low-fill design, confirm the following for the exact product in question, in writing:
- The particle-size distribution, including the fines fraction, and how it is controlled batch to batch.
- The recommended and minimum fill levels, and the basis for those figures — mass, settled height, or both.
- Whether the media is intended for the specific application, and what the supplier’s documented application limits are.
- Whether the product is approved for potable water contact in your destination market. A “food grade” description is not the same as drinking-water suitability; that must be verified for the exact product, the application conditions, and the market where it will be installed.
- Retention recommendations, if any: aperture guidance, retainer type, and orientation constraints.
- End-of-life criteria, so that the minimum fill level used in your verification matches the point at which the media is meant to be replaced.
FAQs
Can I verify restraint with a weight check alone?
No. At low fill levels, dissolution and particle escape both reduce media mass, and a weight check cannot separate them. Pair downstream particle capture with a separate dissolved-phosphate measurement, or run the test under conditions where dissolution is negligible relative to your weighing resolution.
Is a finer retention mesh always the safer choice?
Not automatically. A finer mesh blocks smaller particles but also raises differential pressure, can blind quickly with fines and precipitated material, and may change flow distribution through the bed. The correct aperture is the one that blocks the smallest particle in the actual batch while remaining compatible with the housing’s pressure and flow requirements.
Does low fill level affect scale-inhibition performance?
Restraint and performance are different questions. A low fill reduces the amount of media available and can create bypass paths that shorten contact with the water, but whether performance is still adequate depends on the application, the water conditions, and the supplier’s guidance for that specific product. Do not assume that passing a restraint check also confirms treatment performance.
Does food-grade certification mean the media is suitable for drinking water?
No. Food-grade status describes one aspect of material compliance and does not by itself establish potable-water suitability. Drinking-water approval depends on the exact product, the contact conditions, and the regulations of the destination market, and should be confirmed in writing for each of those.
Requesting the right information from a supplier
ENVO CHEMICAL can discuss polyphosphate media and cartridge restraint questions where the application and specification are clear. To get a useful answer rather than a generic one, include the following with your inquiry: the equipment or cartridge type and its orientation; the intended fill level and how you define it; the minimum fill level you plan to allow; the source-water conditions relevant to the application, such as temperature, pH, and hardness, if known; the design flow rate and pressure range; the particle-size or aperture specification you are working to; your technical objective, whether that is preventing media escape, eliminating bypass, or establishing an end-of-life criterion; the quantity you are evaluating; and the destination market, so that any compliance question can be addressed against the correct requirements.
