
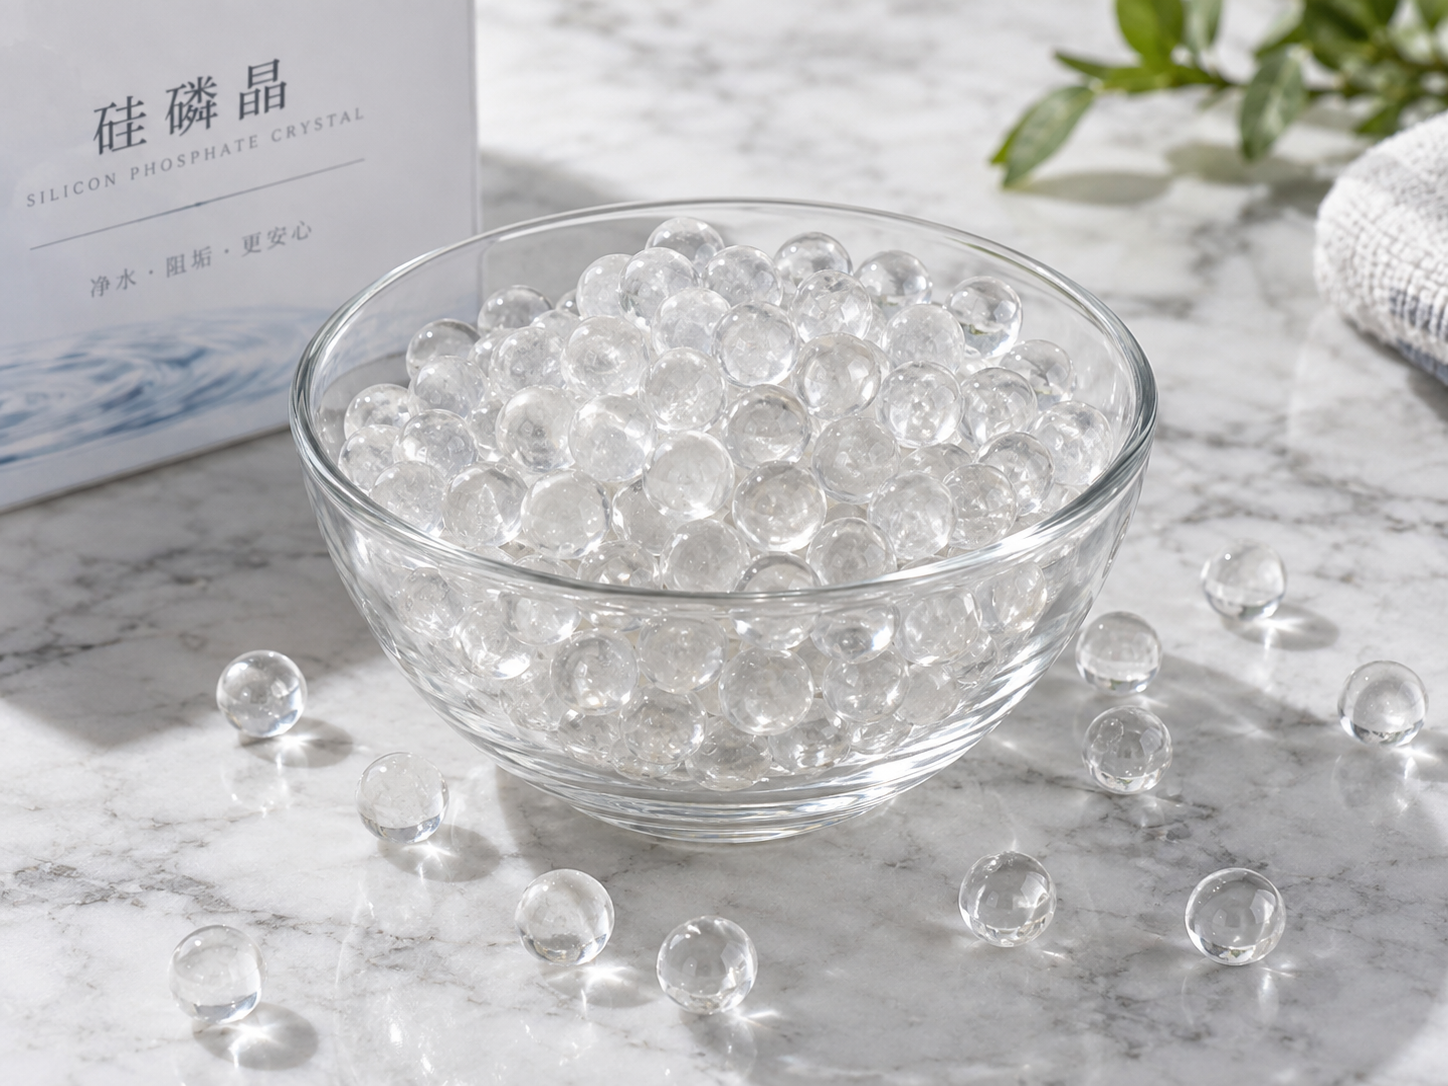
What operator agreement means in Siliphos media appearance grading
Operator agreement is the degree to which two or more inspectors, grading the same sample under the same conditions, reach the same grade. It is not a personality trait or a training certificate — it is a measurable property of your inspection system. If you want a defensible appearance grade for Siliphos media, you have to define the attributes, fix the viewing conditions, run a blind round-robin, and calculate the agreement. Agreement you have not measured is agreement you cannot claim.
This matters most to people who buy, receive, or release phosphate-based water-treatment media: filter and cartridge manufacturers, water-treatment equipment builders, importers, distributors, and QC staff who sign off incoming lots. Appearance is usually the first and cheapest check performed on a delivery, which is exactly why it needs to be repeatable rather than intuitive.
Why appearance grading drifts between operators
Disagreement rarely comes from carelessness. It comes from ambiguity. The most common causes are:
- Undefined attributes. “Looks normal” is not a grade. Colour, transparency, shape, surface condition, fines, and foreign matter are separate judgement calls and need separate definitions.
- No physical reference. Two operators mentally comparing a sample to two different remembered lots will always test the limits of language.
- Uncontrolled lighting. The same crystals read differently under cool white LED, warm indoor light, and open shade. Colour and haze judgements are especially sensitive.
- Different viewing geometry. Looking down into a deep bag versus spreading a single layer on a tray changes what is visible, including dust and broken pieces.
- Order effects. After a badly broken lot, the next normal lot looks excellent. After a pristine sample, a normal lot looks poor.
- Motivation asymmetry. A supplier’s inspector and a receiver’s inspector may have different thresholds for calling a defect.
Step 1: Define the attributes before you grade anything
Write the attribute list from the supplier’s specification for the exact grade being supplied, then split it into things a human eye can honestly judge and things it cannot. Do not carry attribute definitions from one product to another: Siliphos, siliphos crystal, phosphate crystal, and generic polyphosphate media are not automatically interchangeable, and neither are their acceptance criteria.
| Appearance attribute | How it is judged | What it indicates — and what it does not |
|---|---|---|
| Colour and uniformity | Against a retained master sample, under defined light | Batch-to-batch consistency and possible contamination or moisture uptake. Does not confirm phosphate content or dissolution behaviour. |
| Transparency / haze | Visual, single layer, fixed background | Surface condition and manufacturing consistency. Not a performance specification. |
| Shape regularity | Proportion of irregular or deformed pieces | Forming or handling quality. Not a measure of scale-inhibition capacity. |
| Broken pieces and fines | Visual estimate plus, where required, a sieve check | Handling, transport, or attrition damage; relevant to flow and pressure behaviour in a housing. Particle size distribution itself belongs to a sieve test, not to the eye. |
| Foreign matter | Visual scan of a spread sample | Contamination risk. A pass here does not establish suitability for any particular water application. |
| Caking / surface moisture | Visual and tactile, recorded separately | Packaging and storage conditions. Not a measure of chemical performance. |
Keep the scale short — typically pass / marginal / fail, or a three- or four-point ordinal scale. Add an explicit “cannot judge” option so that uncertainty is recorded rather than forced into a wrong grade. Note that appearance grading is an inspection step, not a functional test. Scale inhibition, corrosion inhibition, softening, filtration, and disinfection are different functions; none of them can be verified by looking at crystals.
Step 2: Build a physical master reference set
Agreement depends on a shared physical benchmark, not a shared description. A workable master set includes:
- An acceptance master — sealed, dated, labelled with the specification it represents.
- Boundary examples — one sample just inside and one just outside acceptance, so operators calibrate their threshold rather than only their “good” eye.
- Rejection examples — typically discolouration, heavy fines, visible foreign matter, or caking.
- A defect photo or drawing sheet keyed to the same labels used in the record form.
Store masters away from light and moisture, and replace them on a defined cycle. An aged master that has yellowed will quietly shift the whole inspection system.
Step 3: Control the viewing conditions
This is the step most plants skip, and it is often the reason agreement is poor even after training. Standardise and write down:
- Light source type and colour temperature, and a recorded illuminance level that can be reproduced at the bench;
- A matte, neutral background — white or mid-grey, never a coloured tray;
- Sample presentation: quantity, single-layer spread, clean dry tray, same tray for every operator;
- Viewing distance and angle, and whether the judgement is made with the sample wet or dry;
- Whether any magnification is permitted, and if so, which lens;
- Time limit per sample, so that fatigue affects everyone equally.
If your customer inspects under different conditions, agree in writing whose conditions govern, or expect recurring disputes at receiving.
Step 4: Run a blind agreement trial
Select a set of samples that spans the range you actually see: clearly acceptable, clearly unacceptable, and several borderline lots. Give every operator the same set in a randomised order, without knowing the reference grade or each other’s results, and without discussion during the trial. Include at least some samples twice, under different codes, to detect self-inconsistency as well as disagreement between people.
Sample count and lot sampling should follow your own quality plan; if your QMS uses an attribute sampling scheme such as ISO 2859-1, the appearance categories must be defined as attributes before the scheme can be applied. Do not borrow sample sizes from another product’s specification.
Step 5: Calculate agreement, not just consensus
Two numbers are useful. Percent agreement for each attribute equals the number of matching judgements divided by the total number of paired judgements, multiplied by 100. It is easy to read but ignores chance agreement.
Cohen’s kappa corrects for chance: kappa = (observed agreement − expected agreement) ÷ (1 − expected agreement). For three or more operators, use Fleiss’ kappa; for ordinal scales, use a weighted kappa so that a one-step disagreement counts less than a two-step one. Many QC groups use the descriptive bands published by Landis and Koch as a rough convention:
| Kappa value | Conventional interpretation |
|---|---|
| Below 0.00 | Poor — worse than chance |
| 0.00 – 0.20 | Slight |
| 0.21 – 0.40 | Fair |
| 0.41 – 0.60 | Moderate |
| 0.61 – 0.80 | Substantial |
| 0.81 – 1.00 | Almost perfect |
Interpret the numbers by attribute, not just overall. A team can agree well on foreign matter and badly on haze, which points to a specific definition problem rather than a general training problem. Also look at the direction of disagreement: if one operator consistently grades one step stricter, that is a calibration issue; if disagreements scatter randomly, the attribute definition is probably too vague.
Step 6: Retrain, re-verify, and record
Close the loop with targeted action. Rewrite the ambiguous attribute, add a new boundary master, re-brief the operators together using the master set, then repeat the blind trial. Keep a dated record for each operator showing the trial, the calculated agreement, and the corrective action. Re-run the trial when a new operator joins, when a new supplier or grade is introduced, after any change in lighting or sample presentation, and on a routine interval set by your quality plan.
Checklist: signs your grading programme is not yet under control
- Two inspectors can disagree on the same sample and neither can point to a written rule.
- Grading depends on which operator is on shift that day.
- Lighting or trays are borrowed from another bench and changed without notice.
- The master sample set is more than a few years old, or has been stored in sunlight.
- Disagreements are settled by seniority rather than by reference to a calibrated boundary sample.
- No agreement figure has ever been calculated for any attribute.
Frequently asked questions
Can two operators disagree and both be right?
Only if the grade boundary is undefined. Once a boundary master exists, a judgement is either inside or outside acceptance, and disagreement becomes a calibration error rather than a difference of opinion.
Is colour a reliable grading attribute?
Colour is useful for detecting lot-to-lot variation and possible contamination, but it is highly sensitive to lighting and to the age of the reference. It should be one attribute among several, not the whole grade.
How often should agreement be re-checked?
Set the interval in your quality plan. The events that reliably require a re-check are operator turnover, a new supplier or product grade, a change in viewing conditions, and a rise in customer complaints about appearance.
Does uniform appearance mean better scale-inhibition performance?
No. Uniform appearance suggests consistent manufacturing and handling, but scale inhibition, corrosion control, and any drinking-water suitability claim must be established for the exact product from the supplier’s specification and, where required, verified test data. A description such as “food grade” does not by itself confirm that a product is approved for drinking-water use in a given market.
Getting the basis of your inspection plan right
An appearance grading system is only as good as the specification behind it. Before you finalise attribute definitions or acceptance masters for a specific Siliphos grade, you need that grade’s own declared characteristics, packing format, and intended application — not a generic description. ENVO CHEMICAL can provide the product-specific information that your inspection plan should reference, so your operators are calibrating against the correct baseline.
If you would like help aligning your grading criteria with a specific material, send us the product grade you are working with, your application and equipment type, the source-water conditions where relevant, the specification or acceptance criteria you currently use, your required quantity and destination market, and the technical objective you are trying to meet. With those details, the discussion can stay focused on the attributes that genuinely affect your acceptance decision.
