
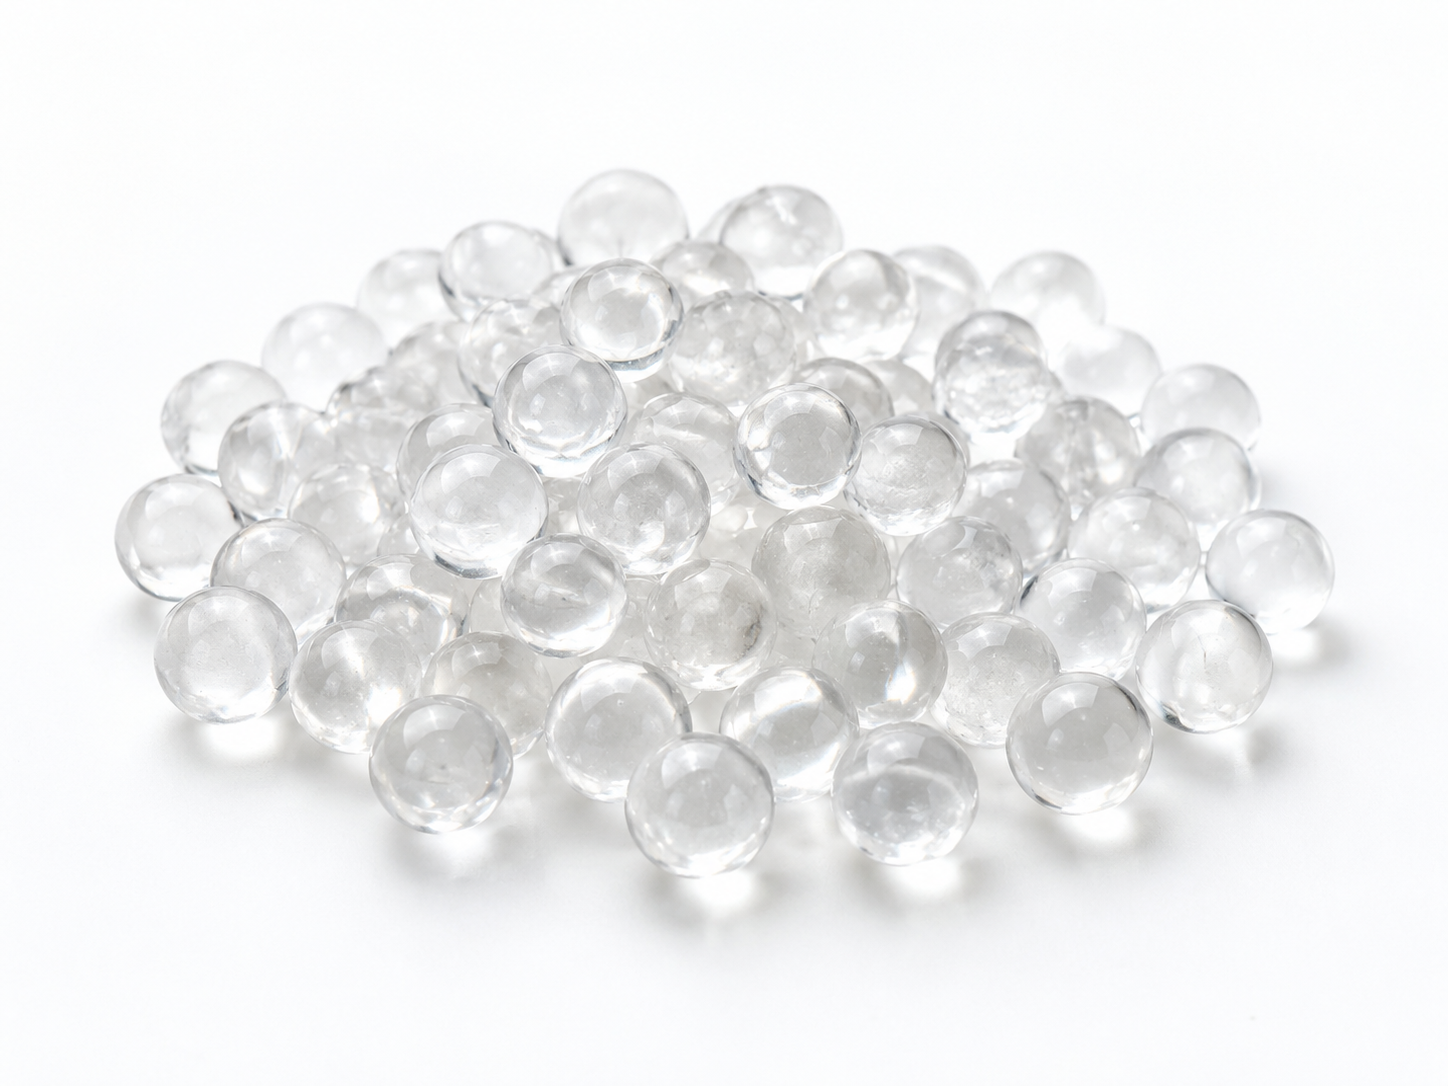
Why Critical and Cosmetic Defect Limits Must Be Treated Differently in Polyphosphate Products
Polyphosphate inspection should assign separate acceptance criteria to defects that impair scale-inhibition performance and those that affect only appearance. Critical defects — such as irregular dissolution rates, contaminated particle surfaces, or inconsistent crystal size distribution — directly reduce the material’s ability to sequester hardness ions and protect downstream equipment. Cosmetic defects — including minor surface discoloration, slight size variation within an acceptable range, or minor packaging blemishes — do not compromise the phosphate’s threshold or sequestration function. Merging both categories into a single pass-fail rule either rejects usable product or accepts material that will fail in service.
This distinction matters most for procurement teams, filter-cartridge manufacturers, and water-treatment system integrators who receive polyphosphate media in bulk and must decide quickly whether a lot is fit for installation. The sections below explain how to define each category, what to look for during incoming inspection, and how to document findings that protect both product quality and supply-chain efficiency.
Understanding What Polyphosphate Media Actually Does — and What It Does Not Do
Before setting defect limits, it helps to clarify the functional role of polyphosphate crystals such as siliphos-type products. These materials are scale-inhibition agents, not water softeners, scale removers, or disinfectants. They work by releasing orthophosphate and long-chain polyphosphate ions into the water stream, where those ions interfere with crystal nucleation of calcium carbonate and other sparingly soluble salts. The result is a threshold effect that keeps hardness minerals in a dispersed, non-adhering state.
Because the mechanism is chemical release rather than physical filtration or ion exchange, the quality of the crystal itself — purity, dissolution behaviour, particle integrity — determines whether the product performs as specified. A chip on a crystal face may be cosmetic. A crystal contaminated with foreign particulates that alter dissolution kinetics is not.
Defining Critical Defects in Polyphosphate Inspection
What counts as a critical defect?
A defect is critical when it has a demonstrable or high-probability impact on the polyphosphate’s ability to inhibit scale under the conditions for which it was selected. The following categories typically fall into this group:
- Contamination or foreign inclusions: Visible non-phosphate particles embedded in or adhering to crystals. These may introduce unwanted ions or physically block dissolution.
- Abnormal dissolution rate: Crystals that dissolve too quickly (wasting dosage and reducing service life) or too slowly (failing to maintain the required phosphate residual in the treated water).
- Severe size inconsistency: A particle-size distribution so wide that fine dust passes through the media bed while oversized chunks create channelling or uneven flow.
- Moisture damage or caking: Clumping caused by improper storage that prevents free-flowing behaviour and makes metering unreliable.
- Colour or odour anomalies indicating chemical degradation: Discoloration beyond normal batch variation can signal partial hydrolysis or exposure to incompatible substances.
Each of these issues can lead to under-dosing, equipment fouling, or customer complaints downstream. When any one is confirmed, the lot should be quarantined and evaluated against the supplier’s technical data sheet — not against a generic appearance standard.
Defining Cosmetic Defects in Polyphosphate Inspection
Cosmetic defects are those that a qualified inspector can identify by sight or simple touch but that do not, on their own, affect the phosphate’s threshold inhibition performance. Typical examples include:
- Minor surface roughness or matte finish variation from batch to batch.
- Slight colour shade differences that remain within the supplier’s stated normal range.
- Small chips on crystal edges that do not change the overall particle-size distribution.
- Dust or loose fines on the surface of a sealed container that can be removed without affecting the bulk product.
- Label or packaging print irregularities that do not obscure lot identification or handling instructions.
Cosmetic defects should be recorded for trend analysis and supplier feedback, but they should not trigger automatic rejection unless they exceed a pre-agreed tolerance that the buyer has formally documented in the purchase specification.
How to Build a Two-Tier Inspection Protocol
A practical inspection workflow separates the two defect classes at the point of receiving goods. The table below summarises a structure that procurement and quality teams can adapt to their specific application.
| Inspection Step | Critical-Defect Check | Cosmetic-Defect Check |
|---|---|---|
| Documentation review | Verify certificate of analysis, lot number, and storage conditions against purchase order. | Confirm packaging integrity and label completeness. |
| Visual sampling | Inspect a representative sample for foreign matter, caking, or abnormal colour. | Note surface texture, chip frequency, and colour shade within the normal band. |
| Physical testing | Perform dissolution-rate test or particle-size analysis if specified in the contract. | Measure bulk appearance attributes only if a tolerance has been agreed. |
| Decision | Fail the lot if any critical defect is confirmed; request supplier investigation. | Accept with noted observations or reject only if cosmetic tolerance is exceeded. |
The key is to write these two paths into the same inspection plan so that the warehouse or receiving team does not apply a single blanket rule. Training should emphasise that a slightly rough-looking crystal is not automatically a failed crystal — but a crystal that smells off or will not dissolve at the expected rate is a different matter entirely.
Common Pitfalls When Inspecting Polyphosphate Media
Even experienced buyers encounter problems when defect criteria are vague. Three recurring mistakes deserve attention.
- Treating all discoloration as critical. Polyphosphate crystals can vary in shade depending on raw-material source and manufacturing batch. Without a documented reference sample or stated colour range, inspectors may reject acceptable product.
- Ignoring dissolution behaviour. Visual inspection alone cannot confirm whether the phosphate will release at the correct rate. If the application demands a specific dosage or residual, a simple dissolution check in representative water is essential — and that test belongs in the critical-defect column, not the cosmetic one.
- Applying the same standard to different product forms. Siliphos-type crystals, liquid polyphosphate solutions, and granular polyphosphate blends each have different failure modes. A defect limit written for one form should not be copied to another without technical justification.
What to Confirm Before Finalising Your Defect Limits
Because polyphosphate performance depends on water chemistry, temperature, flow rate, and contact time, no universal defect table can replace application-specific validation. Before locking in critical and cosmetic thresholds, confirm the following with your supplier or internal engineering team:
- The target phosphate residual and the dosage required to maintain it in your specific water matrix.
- The acceptable particle-size range for your dosing equipment or media vessel.
- Whether the product carries any third-party certification or test data that defines baseline quality.
- The storage and shelf-life conditions that the supplier guarantees, so you can distinguish degradation from original-quality variation.
- Whether the product is intended for potable-water contact, and whether that status has been verified for the destination market’s regulatory framework — not assumed from a “food grade” label alone.
Documenting these points ensures that your inspection criteria are tied to real performance requirements rather than arbitrary appearance preferences.
Frequently Asked Questions About Polyphosphate Defect Inspection
Can a single lot contain both critical and cosmetic defects?
Yes. A batch may have a few chipped crystals (cosmetic) alongside a cluster of caked material (critical). The inspection protocol must evaluate each finding against its own category and apply the appropriate decision — quarantine for critical issues, notation for cosmetic ones.
Do I need laboratory testing for every incoming shipment?
Not necessarily. Routine visual and physical checks can cover cosmetic and obvious critical defects. Dissolution testing or chemical analysis should be performed on a sampling plan — for example, the first lot from a new supplier, then periodically — unless your contract specifies every-shipment verification.
Who should define the defect limits — the buyer or the supplier?
Both parties should agree. The supplier provides technical data and normal-range specifications; the buyer translates those into inspection tolerances that reflect the actual application. A purchase specification that references the supplier’s data sheet is the most defensible approach.
Is a minor smell change always a critical defect?
Not automatically, but it should trigger a critical-defect investigation. Polyphosphate should have little to no odour. A noticeable smell may indicate contamination, moisture exposure, or partial chemical breakdown, all of which require further testing before the lot is released.
Ready to Refine Your Polyphosphate Quality Criteria?
If you are sourcing polyphosphate scale-inhibition media and need to align your receiving inspection with the actual demands of your water-treatment system, the next step is to match defect limits to your operating conditions. Share your application type (drinking water, commercial RO pretreatment, industrial cooling, etc.), your source-water hardness and pH range, the equipment or dosing format you use, and the quantity you plan to order. ENVO CHEMICAL can then help you confirm which product specifications and test data are relevant to building a two-tier inspection plan that protects both performance and supply efficiency.
