
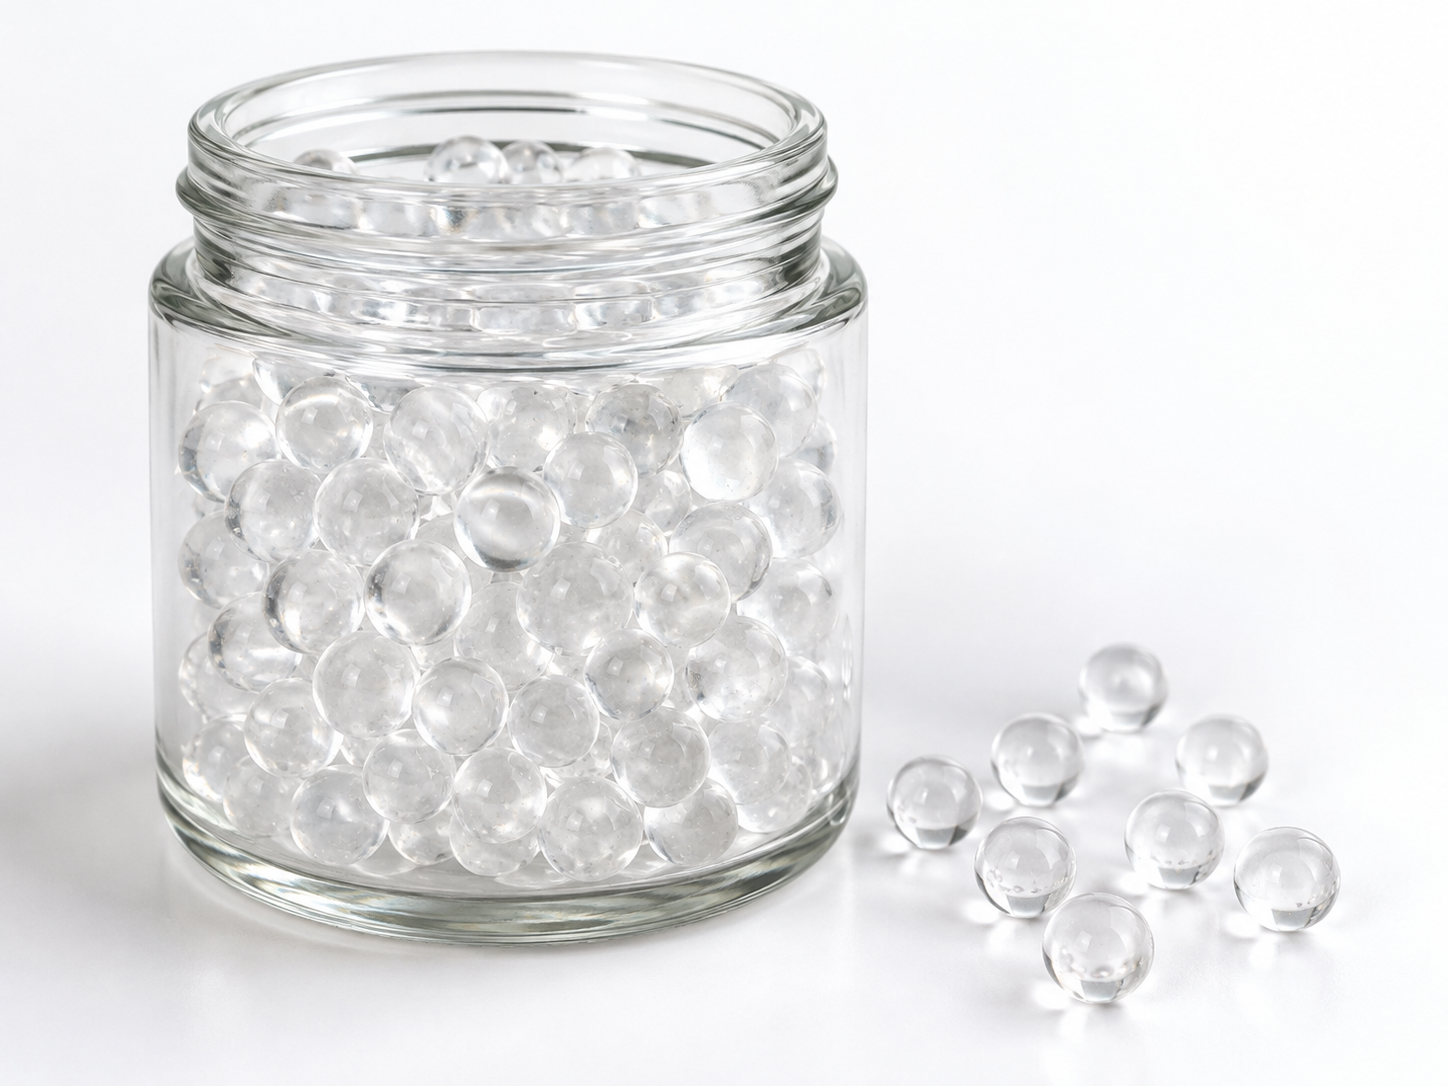
Can Automated Vision Inspection Reliably Sort Polyphosphate Ball Defects?
Automated vision inspection can reliably sort many common defects in polyphosphate balls—such as surface cracks, color inconsistencies, size deviations, and foreign-matter contamination—provided the system is calibrated to the specific optical and geometric properties of the media and the inspection line is designed for the throughput and defect-severity profile of the production batch. However, no single camera-based system catches every flaw without trade-offs in speed, cost, or false-reject rate. Reliability depends on lighting, algorithm training, defect classification priorities, and how “defect” is defined for the end use.
This matters because polyphosphate media (including siliphos-type crystals) serve as scale-inhibition and corrosion-control agents in residential, commercial, and industrial water-treatment systems. A ball that chips, discolors, or varies in diameter can alter dissolution behavior, reduce dosing accuracy, and introduce particulates downstream. Buyers, packagers, and OEM integrators need to know whether machine vision is a practical gatekeeper—or whether supplementary manual or statistical checks remain necessary.
What Defects Actually Matter in Polyphosphate Balls
Not every visual imperfection compromises performance. Before deciding on an inspection method, classify the defects that are functionally relevant versus those that are merely cosmetic.
- Surface cracks and fractures: These create fines that can clog dosing equipment or bypass filters. Cracks also accelerate dissolution, shortening media life unpredictably.
- Color variation: Shifts from the typical translucent or pale hue may signal incomplete polymerization, contamination, or thermal stress during production. Color alone does not always predict function, but it is a fast proxy for process drift.
- Size and shape out-of-tolerance: Balls that are too large may not dissolve at the designed rate; balls that are too small may pass through retainer screens. Sphericity affects packing density in cartridges.
- Surface contamination or inclusions: Foreign particles embedded in or adhering to the ball can introduce unwanted minerals or organics into the treated water stream.
- Cloudiness or internal voids: These may indicate trapped moisture or poor raw-material blending, potentially affecting long-term stability.
A vision system must be tuned to detect the subset of these that the quality plan prioritizes. Trying to flag every anomaly at production speed usually results in excessive false rejects, which raises cost without improving protection.
How Automated Vision Inspection Works for Spherical Media
Core components of a typical system
A machine-vision sorting line for polyphosphate balls generally includes a feed mechanism that singles and orients the media, one or more cameras (often a combination of area-scan and line-scan), controlled illumination, and a reject actuator (air jet, mechanical arm, or diversion gate). Software performs defect detection, classification, and decision-making in real time.
The key variables that determine whether the system works well for this specific product:
- Optical properties: Polyphosphate balls can be translucent, glossy, or slightly refractive. Specular highlights from overhead lighting can mask surface cracks. Diffuse or multi-angle lighting setups are typically required.
- Size range: Most siliphos-type crystals fall in a relatively narrow diameter band (often 2–6 mm or similar, depending on grade). The camera resolution and field of view must resolve features at that scale without blurring adjacent balls.
- Throughput: High-speed lines (hundreds of balls per second) may rely on line-scan cameras and statistical sampling rather than inspecting every single unit.
- Defect library: The algorithm needs training images of known-good and known-bad samples. For a product with subtle defect types, building this library can be the most time-consuming step.
What the technology can do well
When set up correctly, automated vision excels at:
- Consistent detection of gross geometric defects (oversized, undersized, misshapen units)
- Rapid color-sorting to separate off-hue batches
- Identification of obvious surface cracks and chipped edges
- Removal of foreign objects that differ in color or texture from the media
These capabilities make vision inspection a strong first-pass filter, especially when integrated with weight-based or near-infrared checks for properties that cameras cannot see (such as internal moisture content or exact phosphate-chain length).
Where reliability drops
Several practical limits affect confidence in a vision-only approach:
- Internal defects: Voids, inclusions, or compositional variations hidden beneath the surface are invisible to standard cameras unless paired with X-ray or hyperspectral imaging, which adds cost.
- Subtle dissolution-relevant flaws: A hairline crack that does not yet shed fines may be invisible at speed but still problematic over months of service.
- Lighting sensitivity: Small changes in ambient light or lamp aging can shift defect thresholds, requiring frequent recalibration.
- Algorithm drift: If the raw material or production process changes slightly, the trained model may start misclassifying good balls as defective, or vice versa.
For these reasons, most serious quality programs treat vision inspection as one layer in a multi-stage control plan rather than the sole decision point.
Comparing Inspection Approaches for Polyphosphate Media
| Method | Best at detecting | Limitation | Typical role |
|---|---|---|---|
| Automated vision (visible light) | Surface cracks, size, color, foreign objects | Cannot see internal structure; sensitive to lighting | High-speed first-pass sorting |
| Near-infrared (NIR) spectroscopy | Composition, moisture, polymer chain indicators | Slower per unit; higher equipment cost | Compositional verification on samples or in-line |
| X-ray or CT imaging | Internal voids, density anomalies, inclusions | Very high cost; low throughput | Periodic audit or R&D validation |
| Manual visual inspection | Ambiguous or borderline cases | Subjective; slow; fatigue-prone | Secondary check or small-batch QC |
| Statistical process control (SPC) on dissolution tests | Functional performance over time | Not real-time; destructive or slow | Batch release validation |
The most reliable programs combine at least two of these: vision for speed and geometric sorting, plus a slower compositional or functional test to confirm that the balls meeting visual criteria also perform as expected in water.
Practical Guidance for Buyers and Integrators
If you source polyphosphate balls and need to evaluate whether the supplier’s inspection process is adequate, ask for specifics rather than accepting a blanket claim of “automated inspection.”
- What defect types are the cameras trained to detect? Request the defect classification list.
- What is the reject rate and the false-reject rate? A system that discards 15 % of good product to catch 95 % of bad product may not be economical.
- Is there a complementary test—dissolution rate, phosphate content, leachate analysis—performed on each batch or on a statistical sample?
- How often is the vision system recalibrated, and against what reference samples?
- Does the inspection cover 100 % of units or a defined sampling plan? Full inspection is preferable for small-lot specialty media; sampling may suffice for large commodity volumes if statistically justified.
For equipment manufacturers who integrate polyphosphate media into cartridges or dosing units, knowing the inspection profile of the media helps you set incoming-quality specifications and decide whether you need your own incoming inspection stage.
Why Defect Control Matters Beyond Aesthetics
Polyphosphate media function by slowly releasing orthophosphate and polyphosphate species into water, where they sequester calcium and other hardness ions and form a thin protective film on metal surfaces. This is scale inhibition and corrosion inhibition—not water softening (which removes hardness permanently) and not disinfection.
A defective ball can disrupt this mechanism in two ways. First, physical degradation (cracking, chipping) releases fines that may be counted as particulate contamination rather than active treatment chemical. Second, compositional inconsistencies (wrong chain length, excess moisture) change the dissolution profile, potentially under-dosing or over-dosing phosphate into the water. Neither outcome is acceptable in applications where dosing accuracy affects compliance or equipment warranty.
This is why the inspection question is not trivial: it is directly tied to whether the media will perform its intended function in the field.
What to Confirm Before Relying on a Vision System
Automated vision inspection is a proven and increasingly affordable tool, but it is not a universal guarantee. Before you treat it as the sole quality gate for polyphosphate balls, confirm the following for your specific grade and application:
- The camera and lighting configuration has been validated against the actual defect types you care about, not just generic surface flaws.
- The algorithm has been trained on representative samples from the production lot, including known-good and known-bad references.
- A functional test (such as a standardized dissolution or leachate test) accompanies the visual sort, at least on a batch basis.
- The system’s maintenance and recalibration schedule is documented and enforced.
- The definition of “defect” aligns with your performance requirements, not just appearance standards.
When these conditions are met, automated vision inspection offers a reliable, repeatable, and scalable way to keep defective polyphosphate balls out of the supply chain. When they are not met, the technology gives a false sense of security.
Next Steps
If you are evaluating polyphosphate media for a water-treatment application—whether for inclusion in a filter cartridge, a dosing system, or a distribution line—and you want to understand the quality-control methods behind the product you receive, share your application details, source-water conditions, required media specifications, and target volume. ENVO CHEMICAL can discuss how its siliphos-type crystal grades are produced and inspected to meet the performance you need.
