
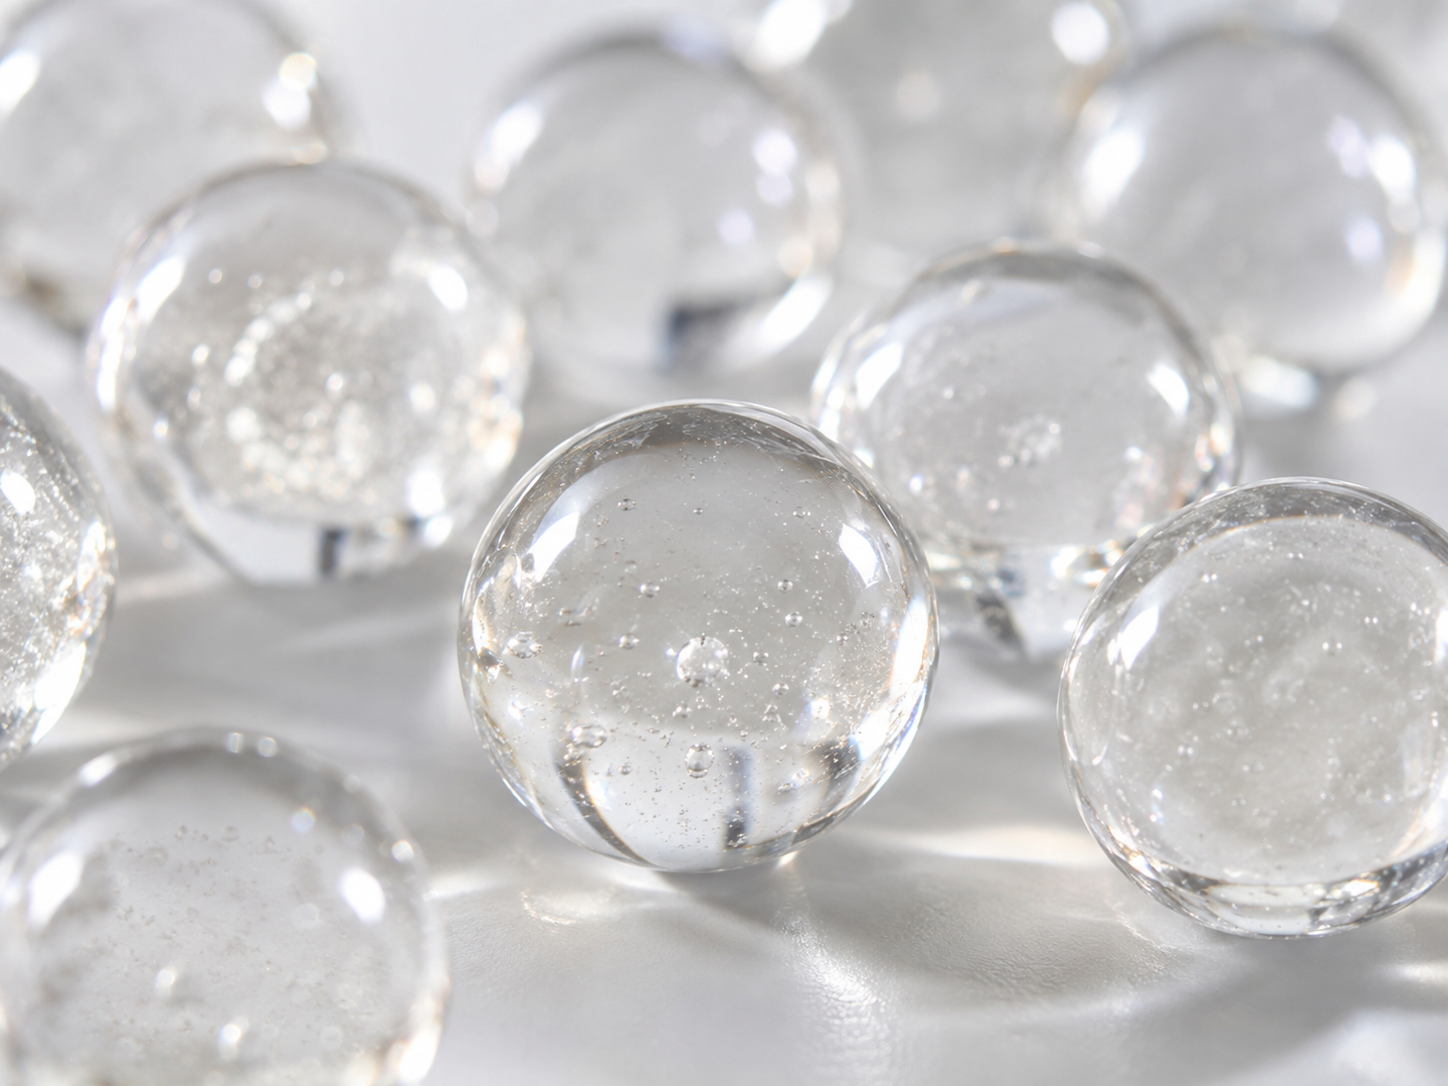
Short Answer
Most internal bubbles in polyphosphate glass are cosmetic — but only under conditions that are worth spelling out. If the voids are small, closed, evenly distributed, and consistent from batch to batch, they do not contact the water and have almost no effect on how the material performs. They become functional — meaning they change behavior you can measure — when they reduce bead density enough to upset volumetric dosing, weaken beads enough to generate fines, break through the surface to change the dissolution area, or vary so much between lots that your dosing stops being predictable.
The practical question is therefore not “are there bubbles?” but “which of the four mechanisms above do these bubbles trigger in my system?” That is what this article works through.
What Internal Bubbles in Polyphosphate Glass Actually Are
Polyphosphate glass — sold under trade names such as Siliphos and more generically as phosphate crystal or polyphosphate media — is an amorphous, water-soluble sodium–calcium phosphate material. The word “crystal” in the trade is commercial shorthand: the material is a glass, not a crystalline solid, produced by melting phosphate raw materials and quenching the melt into beads, spheres, or irregular granules.
Because it is glass, it inherits glass behavior. Gas present in the melt does not escape cleanly during a fast quench. Where that gas is trapped, you get one of three outcomes:
- Closed internal voids — a bubble fully surrounded by solid glass. Water never reaches it until the surrounding material has dissolved away.
- Surface-breaking voids — a bubble that intersects the bead surface, creating a crater or open pore that water reaches immediately.
- Interconnected porosity — a network of connected voids that lets water penetrate well ahead of the normal dissolution front.
Where the gas comes from
Typical sources include air entrained during melting and pouring, water and carbon dioxide released from raw materials as they decompose, reactions between the melt and the crucible or mold surface, and, in some cases, deliberate or incidental additives. Melt viscosity and quench rate matter too: a more viscous melt and a faster quench both make it harder for bubbles to rise and escape before the glass freezes.
This matters because it means some internal porosity is a normal feature of melt-quenched phosphate glass rather than an automatic defect. Two suppliers can both produce sound material with visibly different bubble content.
When Bubbles Stay Cosmetic
Internal voids behave as cosmetic when all of the following hold:
- The voids are small relative to the bead diameter — they don’t dominate the cross-section.
- They are closed, with no path from the void to the surface.
- They are reasonably evenly distributed rather than concentrated in a few beads.
- They occur at a consistent level from lot to lot.
- Measured apparent density, fines content, and dissolution rate stay inside your specification.
Under those conditions the mechanism is simple: polyphosphate glass dissolves from the outside inward. A sealed void in the center has no surface in contact with water, so it contributes nothing to release rate and nothing to reaction chemistry. It reduces the mass of that individual bead slightly, which is compensated for as long as your specification is based on measured density or on dissolution performance rather than on a visual inspection of the beads.
In clear filter housings or consumer-facing products, appearance can be a legitimate commercial requirement in its own right. If a customer sees voids through transparent media, that is a marketing issue, not a water-treatment issue — but it is still a real requirement that belongs in the purchase specification.
When Bubbles Become Functional
1. Density and volumetric dosing
This is the most common way bubbles cause an actual treatment problem. Volumetric feeders and simple cartridge designs dispense by volume. If a lot has a higher internal void fraction, each unit of volume contains less phosphate glass mass, so the same feeder setting delivers less active material. Scale inhibition can then fall short without anything visibly changing in the equipment.
Gravimetric feeders, by contrast, are essentially immune to this effect because they dispense by weight. If your process uses volumetric dosing, apparent density should be a controlled specification, not an afterthought.
2. Mechanical strength and fines
Voids act as stress concentrators. A bead with a large internal cavity or a crack initiated at a void can fracture during bagging, transport, pneumatic conveying, or cartridge filling. The result is fines.
Fines are functionally significant for a specific reason: they dissolve much faster than intact beads because of their far higher surface-area-to-mass ratio. A small quantity of fines can produce a short, high-concentration phosphate release at start-up, which may show up as turbidity, faster-than-expected depletion of the media bed, or premature exhaustion of a cartridge. If you are chasing a “why did this cartridge only last half as long” problem, sieve data and fines content are worth checking before you blame the water chemistry.
3. Surface-breaking voids and release kinetics
A closed void is inert. A void that intersects the surface is not. An open crater adds wetted surface area from day one, which raises the initial dissolution rate. If open porosity is widespread, the release profile changes shape: faster at the start, and often a shorter useful service life overall. Interconnected porosity is the more serious version of the same problem, because water penetrates the bead interior and the structure can begin to break down rather than dissolving smoothly from the outside.
4. Lot-to-lot variability
Here is the point that is easy to miss. A uniformly bubbly product and a clear product can both perform acceptably — but a product whose bubble content swings unpredictably between batches cannot, because you cannot set a feeder or predict a service interval. Variability, not the presence of bubbles, is usually the true defect.
Reading the Symptoms: A Practical Checklist
| What you observe | Likely meaning | What to verify |
|---|---|---|
| Few small closed voids, consistent across lots | Cosmetic | Apparent density, dissolution rate |
| Large single cavity in many beads | Potentially functional — strength and density | Crush or tumble test, apparent density, fines |
| Pitted, matte, or cratered bead surfaces | Functional — open porosity | Fines content, early release, turbidity |
| High fines in the bag or drum | Functional — handling or strength issue | Sieve analysis, conveying method, bead toughness |
| Density drifting between lots | Functional — dosing instability | Lot density record, feeder calibration |
| Visible bubbles only, no measured deviation | Cosmetic unless appearance is a spec | Confirm nothing else has shifted |
How to Evaluate Bubbles Objectively
Visual inspection alone is a poor judge. A bead that looks heavily bubbly may have negligible internal void volume, while a bead that looks clean may contain open porosity. Three measurements do most of the work:
- Apparent (particle) density. Determine the volume of a weighed sample of beads by liquid displacement, then divide mass by volume. Comparing this against the true density of the glass — measured on a crushed, degassed powder — gives a direct estimate of closed internal porosity.
- Bulk density and sieve analysis. Bulk density captures the combined effect of internal voids and packing. Sieving separates intact beads from fines and confirms that the delivered particle size range matches the specification.
- Comparative dissolution testing. Dissolve equal masses of two lots under identical, controlled conditions — same water, temperature, flow, and residence time — and compare phosphate release over time. This is the only test that directly answers “does the bubble content change treatment performance?” Everything else is a proxy.
Where a strength requirement matters, a simple tumble or drop test on a defined sample before and after handling will indicate whether a lot is more prone to generating fines than the material you qualified.
Two Common Misconceptions Worth Clearing Up
Polyphosphate glass is not a water softener. It does not remove calcium and magnesium from water, and it does not regenerate or exchange ions. Its role is scale inhibition through sequestration and crystal-growth interference at low dosage. If your actual goal is hardness removal, you need ion exchange or another removal technology, not phosphate glass. This distinction matters when diagnosing complaints, because a bubbling or fines problem will never explain a hardness reading.
“Food grade” is not the same as “approved for drinking water.” Food-grade raw materials say something about material handling, not about suitability for potable water in a specific market. Potable-water use depends on the exact product, the dosing conditions, and the regulations of the destination market — for example, separate third-party certification schemes exist for drinking-water treatment chemicals in different regions. Confirm this for the specific product and application rather than assuming it from the material description.
Frequently Asked Questions
Are internal bubbles in polyphosphate glass normal?
Yes. Melt-quenched phosphate glass commonly retains some gas as closed voids. The relevant question is whether the void content is controlled and consistent, not whether it exists.
Do bubbles reduce scale-inhibition performance?
Directly, no — a sealed void never contacts water. Indirectly, yes, if the voids lower apparent density enough to underdose a volumetric feeder, or if they weaken beads and create fast-dissolving fines.
Can bubbles clog a filter or cartridge?
Intact beads with internal voids do not clog. Fines generated by bead breakage can, because they migrate, compact, and dissolve rapidly. Check fines content first.
Should I reject a lot with visible bubbles?
Only if measured density, fines content, or dissolution behavior falls outside what you qualified. Rejecting on appearance alone can eliminate perfectly serviceable material — or mask a real density problem that you never measured.
What belongs in the purchase specification?
At minimum: bead size range, fines limit, apparent density range, a defined dissolution test with reference conditions, and an appearance criterion if your market requires one. Add a lot-to-lot consistency clause, since consistency is what actually protects your dosing.
Specifying With Confidence
Internal bubbles should be treated as an engineering variable, not a binary defect. Write density, fines, and dissolution into your specification; measure them on incoming lots; and treat appearance as a separate, market-driven requirement. Then a bubble is only ever a problem when the numbers say so — and when they do, you will know exactly which of the four mechanisms is responsible.
If you are qualifying polyphosphate glass media or comparing lots for a specific system, ENVO CHEMICAL can discuss the parameters that matter for your application. To give a useful answer, please share your application and equipment type (cartridge, feeder, or open bed), feeder mode if applicable, source-water hardness, pH, temperature and flow rate, required bead size or specification, quantity, destination market, and the technical objective — scale inhibition, corrosion-related phosphate dosing, or media replacement in an existing unit.
