
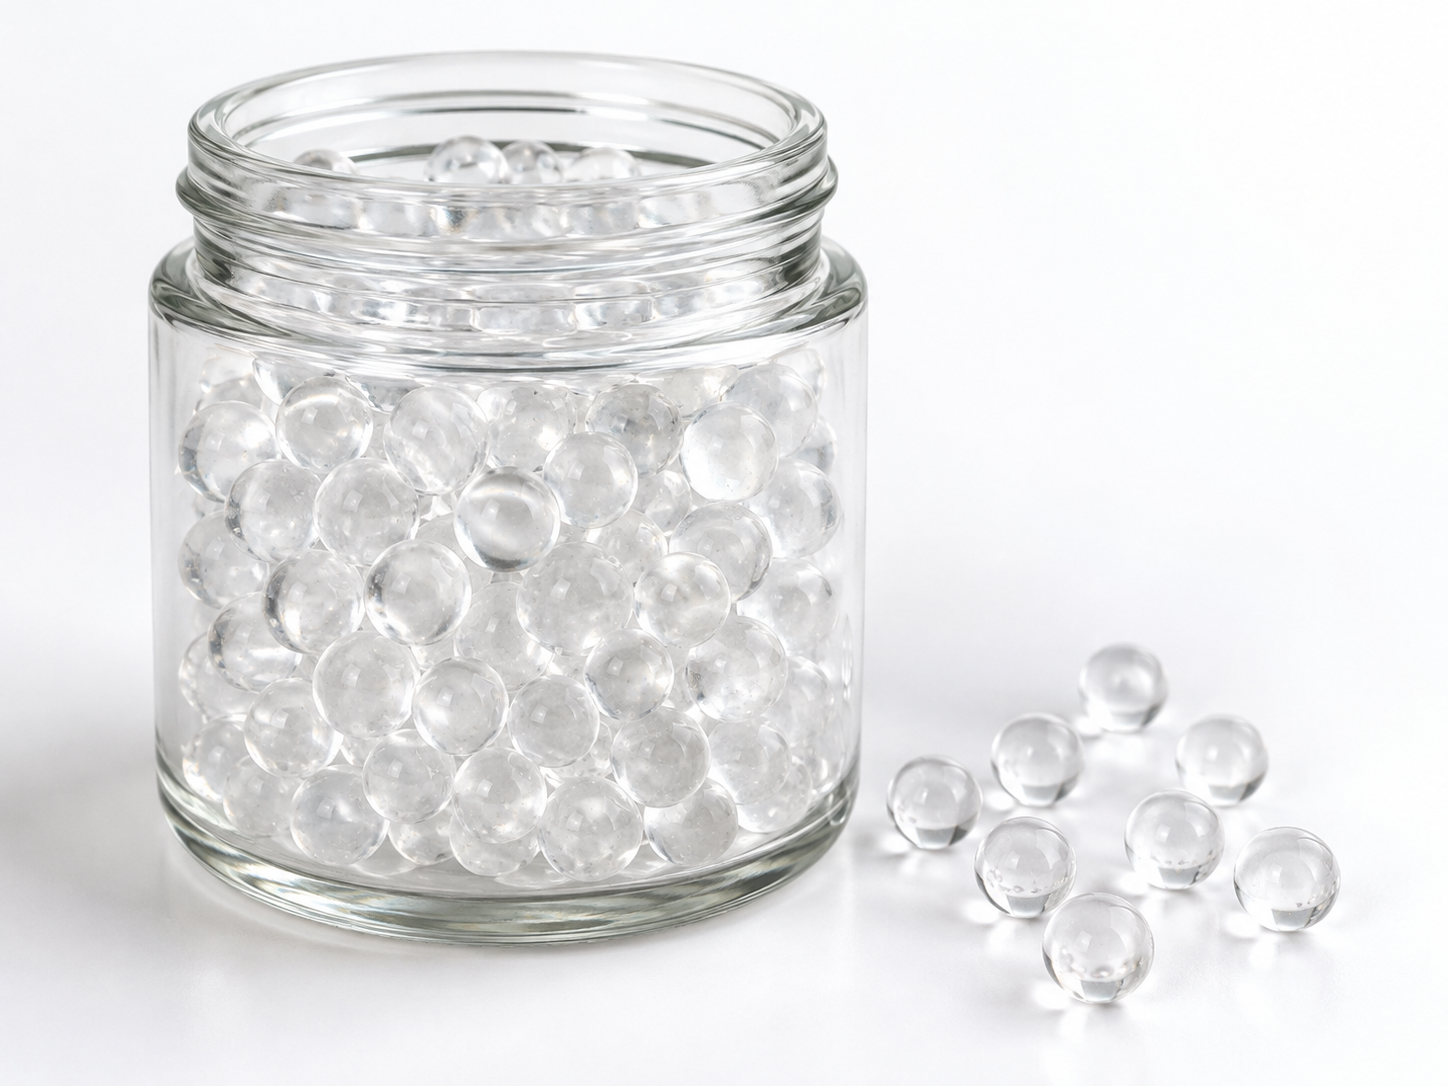
Answer first: treat it as a mechanical failure, not a chemical one
A polyphosphate ball lodged in an outlet screen is documented as a physical containment failure. Before you clear the screen, capture five things: where the beads sit in the housing, the condition of the screen and its retainer, the measured bead diameter against the screen aperture, the operating record (flow, pressure, temperature, time in service), and the material lot code. Those five records carry almost every fault claim, root-cause investigation, and corrective action that follows. Once the screen is wiped clean, most of that evidence is gone.
This matters because polyphosphate crystal is often confused with other media. It releases phosphate species that inhibit calcium carbonate scaling and can help form a protective film on metal surfaces. It is not a softener, it does not remove hardness, it does not filter particulate, and it does not disinfect. A bead stuck in a screen is therefore a sizing, retention, or hydraulic problem — not evidence that the chemistry has failed.
Why polyphosphate balls end up in an outlet screen
The size-match rule between bead and screen
Dissolving polyphosphate glass shrinks over its service life. A screen that retains fresh material at commissioning can become marginal months later, when bead diameters have reduced. If the dispenser was refilled with a different grade, a different nominal size, or a mixed batch, the same effect appears immediately. Measure the lodged beads with a caliper, record the range rather than a single number, and compare it with the screen aperture on the material specification sheet. These are the two numbers that decide whether the installation was correctly matched.
Mechanical and hydraulic causes
- Screen deformation or distortion — a bowed or dished screen has enlarged local apertures even when the nominal mesh is correct.
- Retainer or gasket bypass — beads travel around the screen rather than through it, then collect on the downstream face.
- Flow above the housing’s design range — higher velocity lifts and migrates beads that would otherwise settle.
- Pressure surges or water hammer — a sudden reversal or spike can fluidise the bed and drive material into the outlet.
- Backflow — where no check valve or air gap protects the unit, reverse flow can carry beads into the outlet side.
- Cracked or fragmented beads — fragments are smaller than the parent bead and pass screens that retain whole spheres.
- Vibration and orientation — loosely mounted or horizontally installed dispensers allow the bed to shift against the outlet.
Material and installation causes
- Refilling a serviceable dispenser with an unknown phosphate glass, or with beads from unlabelled packaging.
- Overfilling, which pre-loads the bed against the screen before any flow is applied.
- Thermal exposure above the material’s stated working range, which can soften or agglomerate the glass.
- Agglomeration of adjacent beads into a bridge that then fractures and releases irregular pieces.
Siliphos is a brand name, and polyphosphate glasses are not all interchangeable. Nominal size, dissolution behaviour, and approved application conditions vary by product. Do not assume a replacement grade matches the original unless the specification sheet says so.
Evidence checklist: what to capture and why
| Evidence | How to record it | What it settles |
|---|---|---|
| Beads in situ | Photograph the screen in place, before removal, with a ruler or caliper in frame | Proves the finding is as-found, not created during disassembly |
| Bead dimensions | Caliper measurement of 10–20 individual beads plus any fragments; record minimum, maximum, typical | Establishes whether bead size matched the screen aperture |
| Screen condition | Photograph both faces; measure aperture if possible; note mesh type, distortion, tears, corrosion | Separates a design mismatch from a damaged or wrong component |
| Lot and batch codes | Copy from packaging, cartridge label, or delivery documents | Links the material to its specification sheet and production record |
| Operating record | Flow rate, inlet/outlet pressure, temperature, hours or volume in service, recent changes | Tests hydraulic causes and identifies when the fault began |
| Water data | Hardness, pH, conductivity, and any recent source change | Explains unusual dissolution rate or deposit formation |
| Service history | Commissioning date, refill dates, materials used, who performed the work | Reveals refill errors and grade substitution |
Photograph the fault so it can be interpreted later
Documentation usually fails on images, not words. Take one wide shot that shows the whole installation, one mid shot of the open housing, and one close shot of the screen with a scale reference. Then photograph the removed beads on a plain, matte background beside a caliper reading. Keep lighting flat and avoid flash glare on wet screens, which hides aperture detail. Name the files with the date and equipment tag so that a reviewer a year from now can match each image to the written record.
Preserve the sample correctly
Keep the lodged beads and fragments in a sealed, labelled container. Do not rinse them if surface deposits are part of the question — a rinse removes the very layer that may explain agglomeration or bridging. If you need both clean and as-found material, split the sample and label each part clearly. Record the container, the date, and who removed the material. Where the fault is purely mechanical, laboratory analysis is usually unnecessary; where material identity or grade is disputed, a retained sample is what makes analysis possible at all.
Writing the fault report
A usable report is short and ordered. Use these headings:
- Identification — site, equipment tag, housing or dispenser model, screen part number, material grade and lot code.
- Timeline — commissioning, last refill or service, first observation of the symptom, inspection date.
- Observation — what was found, where in the housing, in plain factual language.
- Measurements — bead size range, screen aperture, pressure and flow at inspection.
- Operating conditions — water data and service history.
- Assessment — the most probable cause, stated as a hypothesis with the evidence that supports it, plus what would confirm or exclude it.
- Immediate action — what was done to restore safe operation, and what was quarantined as evidence.
- Request — what you need from the supplier: specification confirmation, replacement screen, corrected material grade, or a joint investigation.
Write assessment as hypothesis, not verdict. “Bead size range measured 3.1–3.4 mm against a nominal 3.0 mm screen aperture; dissolution over 14 months of service is consistent with the observed carry-over” is far more useful than “the material is defective.”
What a supplier will ask you for
Expect questions about the lot code, the original specification sheet, the screen part number and its measured aperture, the refill history, and the operating data. If the lodged material came from an ENVO CHEMICAL supply, the lot code on the packaging is the fastest route to the corresponding specification sheet, which is why it belongs in the report even when the cause looks obvious. Suppliers cannot evaluate a claim without these records, and a claim without them usually stalls.
Documentation mistakes that weaken a claim
- Clearing the screen before photographing or measuring.
- Reporting a single bead size instead of a range, which hides fragments and mixed grades.
- Recording “screen blocked” without stating which face the beads were on — upstream collection points to sizing; downstream collection points to bypass or deformation.
- Omitting refill records, which are the most common origin of grade and size mismatch.
- Discarding the sample after the unit is returned to service.
- Mixing evidence from two housings in one container, which makes size data meaningless.
Frequently asked questions
Is one lodged bead a functional failure?
Not necessarily. The significance depends on whether the media is intended to be retained, whether flow or pressure drop has changed, and whether downstream equipment or process water is affected. If the unit serves drinking water, confirm suitability for the exact product, dosing conditions, and destination market — food-grade status on a material data sheet does not by itself establish potable-water approval.
Can I simply push the beads back and restart?
You can restore flow that way, but you destroy the evidence and leave the underlying cause in place. Recurrence is likely, and the second event will be harder to diagnose than the first.
Do I need laboratory analysis of the beads?
Rarely for a mechanical lodging. Analysis becomes worthwhile when the dispute concerns the material itself — grade, composition, or whether the correct product was supplied.
How long should I keep the sample?
Until the claim, corrective action, and any warranty discussion are formally closed. Store it dry, sealed, and labelled with the equipment tag and lot code.
Requesting the right support
If you need help identifying a replacement grade, confirming a screen specification, or reviewing a fault report, send the application (potable water, cooling loop, boiler feed, process line), the housing or dispenser model, the screen mesh or aperture, the material grade and lot code, bead measurements, your operating conditions, required quantity, and destination market. With that information, ENVO CHEMICAL can respond to the specific technical question rather than to a general enquiry.
